Get in touch with Suzhou UDTECH Technology Co., Ltd. Company

ISO Certified
Filter Cartridge Equipment Selection
Filter Cartridge Making Machine & Equipment Selection
Compare PP melt-blown, CTO carbon block, string-wound, UDF tube and downstream finishing equipment against the cartridge you need to manufacture—not against isolated catalogue specifications.
Start with the finished cartridge
- Material, ID/OD, length, rating basis, output target, utilities and required finishing decide the line.
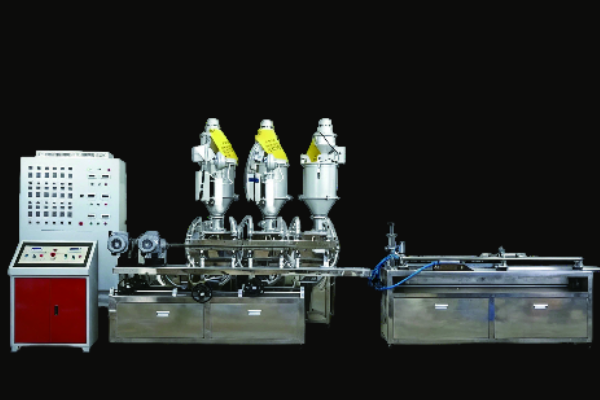
PP melt-blown
2E&2M and 3E&3M routes
CTO carbon block
Mixing through cutting
String-wound & UDF tube
PP yarn and core options & Custom inner diameter review
Finishing scope
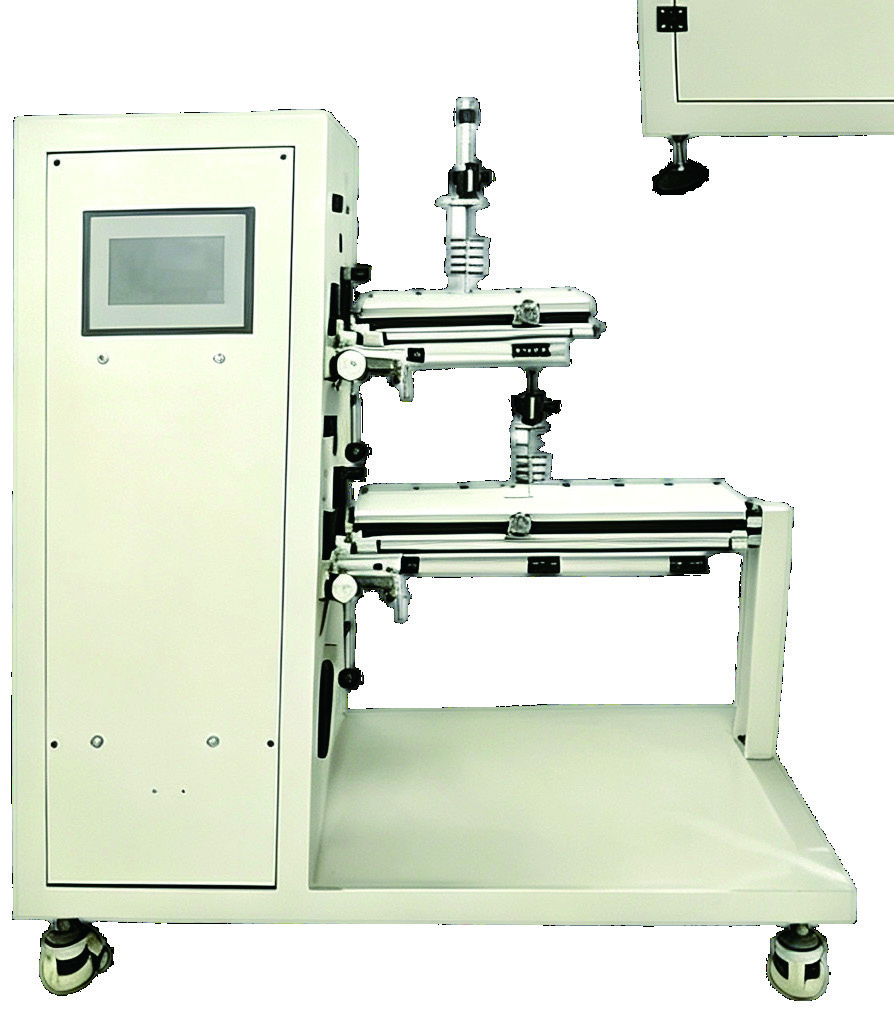
Wrapping, welding, gluing, capping
Filter Cartridge Equipment at a Glance
Evidence boundary:
use a documented requirement and acceptance basis before purchase, consistent with the NIST equipment pre-purchase guide. UDMachine ranges below remain brochure-derived.
Selection boundary
For industrial filtration, water treatment and water filtration projects, the correct filter machine depends on what the cartridge filter must do after manufacture. The production equipment shortlist should connect product geometry, filter media, required process precision, liquid duty, reliability and quality control evidence.
Start with the required filter cartridge, then select the process. Published figures are only a starting point for engineering review; the wrong size, weight basis or downstream scope can make an attractive headline number unusable.
PP melt-blown
3,500–5,800
Published pieces per 24 hours by 2E&2M or 3E&3M configuration, based on 70–200 g cartridges.
CTO carbon block
50–60 sec
Published cycle for one 10-inch cartridge. Carbon granules plus PE feed a mixing, extrusion, cooling and cutting route.
String-wound
60–320 m/min
Published yarn winding speed. Finished good-piece output still depends on length, OD, pattern and changeover conditions.
UDF support tube
20 / 10 kW
Published rated/running power with a 30 m² minimum floor reference and configurable inner diameter.
Finishing module
2,000 W
Published PLC/HMI machine for discharge, nonwoven wrapping, heat welding and finished-product handling.
Capacity comparison rule:
headline output is not comparable until cartridge length, diameter, weight, net runtime and the accepted-piece definition are aligned. Ask for one FAT basis before comparing production lines.
Cartridge Type → Performance Claim → Process → Line Configuration Matrix
This matrix looks in reverse from the sold filter element. It prevents a common assumption: that one filter making machine can manufacture every water filter cartridge or that a machine’s published micron range proves the final filtration claim.
Evidence boundary: the U.S. EPA filtration guide distinguishes rating language and filtration context; it does not validate any machine output shown on this page.
| Target cartridge | Performance brief to define | Forming process | Essential line modules | Acceptance evidence |
|---|---|---|---|---|
| PP melt-blown depth filter | Nominal or absolute rating; particle/challenge method; flow rates, differential pressure, dirt holding capacity and chemical compatibility | Polypropylene melting, extrusion, spinning/deposition, collection, cooling and cutting | 2E&2M or 3E&3M route, collection shaft/tooling, cooling and cut-length control; finishing confirmed separately | Machine: material, dimensions, weight, settings, good-piece rate. Product: application-specific filtration efficiency, structural and material-safety testing. |
| CTO carbon block filter | Carbon grade, binder ratio, density, pressure drop and intended contaminant-reduction claim | Activated carbon and PE mixing, feeding, screw extrusion, cooling and cutting | Mixer, feeder, extruder/workbench, cooling, cutter and dust collection interface | Machine: dimensional consistency and output basis. Product: claim-specific test protocol and lab evidence. |
| String wound filter cartridge | PP yarn, micron rating, winding pattern, core material, length and OD | Controlled yarn winding around a PP or stainless core | Spindle, traverse control, core fixture, tension control and cut/handling method | Pattern, OD, length, weight, line speed, changeover and accepted-piece count. |
| UDF support tube | Tube ID/OD, slot/open-area geometry, stiffness, resin and master batch | PP tube extrusion and downstream handling | Extruder, die/tooling, cooling and sizing route | Drawing-based dimensions, visual criteria and sampled structural checks agreed before build. |
| Finished cartridge assembly | Rod/tube compatibility, nonwoven, adhesive, cap geometry and weld/appearance criteria | Discharge, wrapping, heat welding, gluing, capping and finished discharge | Only the required downstream stations; interface ownership shown in the quote | Cycle observation, bond/weld criteria, dimensional checks and defect log. |
Cartridge Materials, Sizes and Micron Ranges
Material determines the process route. Selecting by appearance alone creates a mismatch risk because PP depth media, carbon block, yarn-wound media and support tubes require structurally different equipment.
Evidence boundary: micron terminology should travel with its rating basis and application conditions; see the U.S. EPA filtration guide. Product dimensions and material ranges here come from the supplied brochure.
PP melt-blown filter cartridges
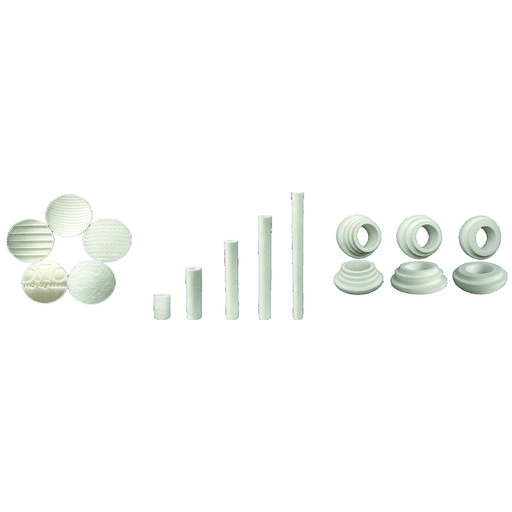
The brochure shows PP spun or melt-blown filter cartridge grades of 1, 5, 10, 20, 30 and 50–100 µm. The default ID is 28 mm, with a published customizable range of 10–150 mm; where the ID is 28 mm, the published OD range is 38–120 mm.
- Confirm virgin/recycled resin rules and color master batch.
- Define single-layer or graded density requirements.
- Keep nominal/absolute wording out of the machine quote unless the test method is named.
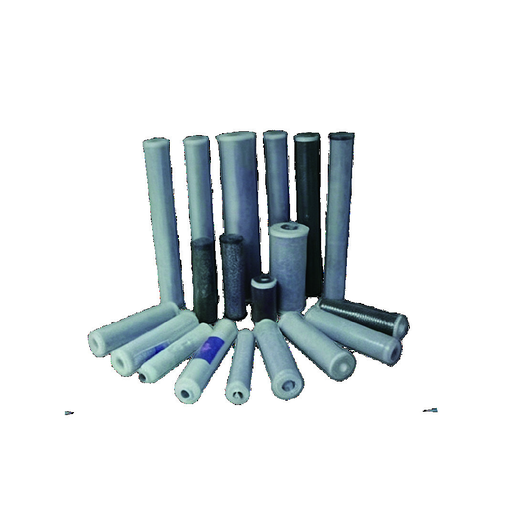
CTO carbon block filter cartridges
The CTO route uses activated carbon granules and PE powder. The brochure shows default 38/63 mm ID/OD, selectable 5, 10, 20 and 30-inch lengths, a 9–100 mm customizable ID range and a 29–150 mm OD range.
- Carbon grade and binder recipe remain product-development inputs.
- Powder properties can change extraction and ignition-control scope.
- A carbon filter cartridge machine cycle does not establish adsorption performance.
Wound filters and support tubes
The wound-filter route uses PP yarn around a PP or stainless-steel core. Published micron grades are 1, 5, 10, 20, 50 and 100 µm. The brochure lists common cartridge lengths of 10, 20, 30, 40 and 100 inches, while the all-in-one winding machine shows a 10–70 inch working range and a 29–150 mm OD range.
Keep media language tied to process
The published UDF tube feed is PP plus master batch, and the inner diameter is customizable. A buyer-approved drawing or sample—not a catalogue description—should control the tooling and extrusion review.
Category terms are not machine routes
In cartridge manufacturing, terms such as spun filter, depth filtration, liquid filtration and pleated filter describe different media or applications. A machine manufacturer should confirm the exact filter cartridge manufacturing route instead of treating every term as interchangeable filter equipment.
Automation and Downstream Finishing Scope
A “fully automatic” label does not necessarily mean that every station required for a sellable cartridge is included in the quote. An unclear line boundary can leave an OEM with a working forming machine and an unexpected manual bottleneck.
Safety boundary: carbon-dust handling must be reviewed against the installed facility and material properties; the OSHA combustible-dust guidance supports that review, not a claim that every carbon mixture presents the same hazard.
Forming core
Material feeding, melt/extrusion or winding, collection/forming and primary control. This is the process heart of the production line.
- Extruder or winding spindle
- Process settings and tooling
- Cooling or collection
Downstream conversion
Cutting, carbon-rod discharge, non-woven wrapping, heat welding, adhesive application, end capping and finished discharge can be separate modules.
- Confirm every interface
- State automatic/manual handoffs
- Name supplied consumables
Facility and safety scope
Utilities, floor layout, guarding and CTO powder controls depend on the installed environment. Carbon dust makes containment, extraction, grounding/bonding, ignition control, electrical classification and housekeeping part of the engineering review.
B
Bronze cost decision card: there is no defensible payback percentage in the available evidence. Compare the installed line by included modules, labor handoffs, tooling, utilities, FAT, training, spares and shipping scope. The cheapest base machine is not always the lowest project cost.
Published Machine Specifications and Selection Limits
This table aligns different brochure formats without filling evidence gaps with estimates. Catalogue values provide a comparison range; the buyer-approved drawing, sample and specification govern the final offer.
Evidence boundary: the comparison keeps unknowns open in line with the NIST equipment pre-purchase guide. Every numeric machine value below is traceable to the supplied brochure.
| Decision row | PP melt-blown | CTO carbon block | PP winding | UDF tube | Finishing |
|---|---|---|---|---|---|
| Model / route | 2E&2M or 3E&3M | Mixing-to-cut line | All-in-one winding machine | Tube extrusion line | Gluing/capping/wrapping machine |
| Raw material | PP / polypropylene | Activated carbon granules + PE | PP yarn; PP or stainless core | PP + master batch | Carbon rods/tubes, nonwoven and adhesive process |
| Length | 10 / 20 / 30 / 40 in | 5 / 10 / 20 / 30 in | 10 / 20 / 30 / 40 / 100 in; machine range shown 10–70 in | Drawing dependent | Compatibility to verify |
| Inner diameter | 28 mm default; 10–150 mm customizable | 38 mm default; 9–100 mm customizable | 28 mm default | Customizable | Compatibility to verify |
| Outer diameter | 38–120 mm where ID is 28 mm | 63 mm default; 29–150 mm range | 29–150 mm | Drawing dependent | Compatibility to verify |
| Decision row | PP melt-blown | CTO carbon block | PP winding | UDF tube | Finishing |
|---|---|---|---|---|---|
| Published micron range | 1 / 5 / 10 / 20 / 30 / 50–100 µm grades | Not stated | 1 / 5 / 10 / 20 / 50 / 100 µm | Not applicable | Not applicable |
| Output / speed | 3,500–4,200 or 5,000–5,800 pcs/24 h by configuration | 1 pc per 50–60 sec for a 10-in cartridge | 60–320 m/min line speed | Not stated | Not stated |
| Output basis | 70–200 g cartridge weight; final size/run basis to agree | 10-in cartridge; other bases to agree | Speed only; good-piece basis to agree | Define from drawing and run-off | Define from rod/tube and operation sequence |
| Rated / running power | 2E&2M: 70 / 28–32 kW; 3E&3M: 100 / 38–40 kW | 16.45 / 8 kW | Motor power depends on size | 20 / 10 kW | 2,000 W |
| Voltage / frequency | Confirm project supply | Confirm project supply | AC 380 V / 50 Hz stated | 380 V / 50 Hz or 220 V / 50 Hz stated | AC 220 V / 50 Hz stated |
| Floor / interface | Layout confirmation required | Mixer, feeder, cooling, cutting and dust scope | Core handling and length clearance | Minimum 30 m² published; line layout to confirm | Upstream/downstream handoffs to confirm |
| Controls | Configuration dependent | Configuration dependent | Configuration dependent | Configuration dependent | PLC + HMI published |
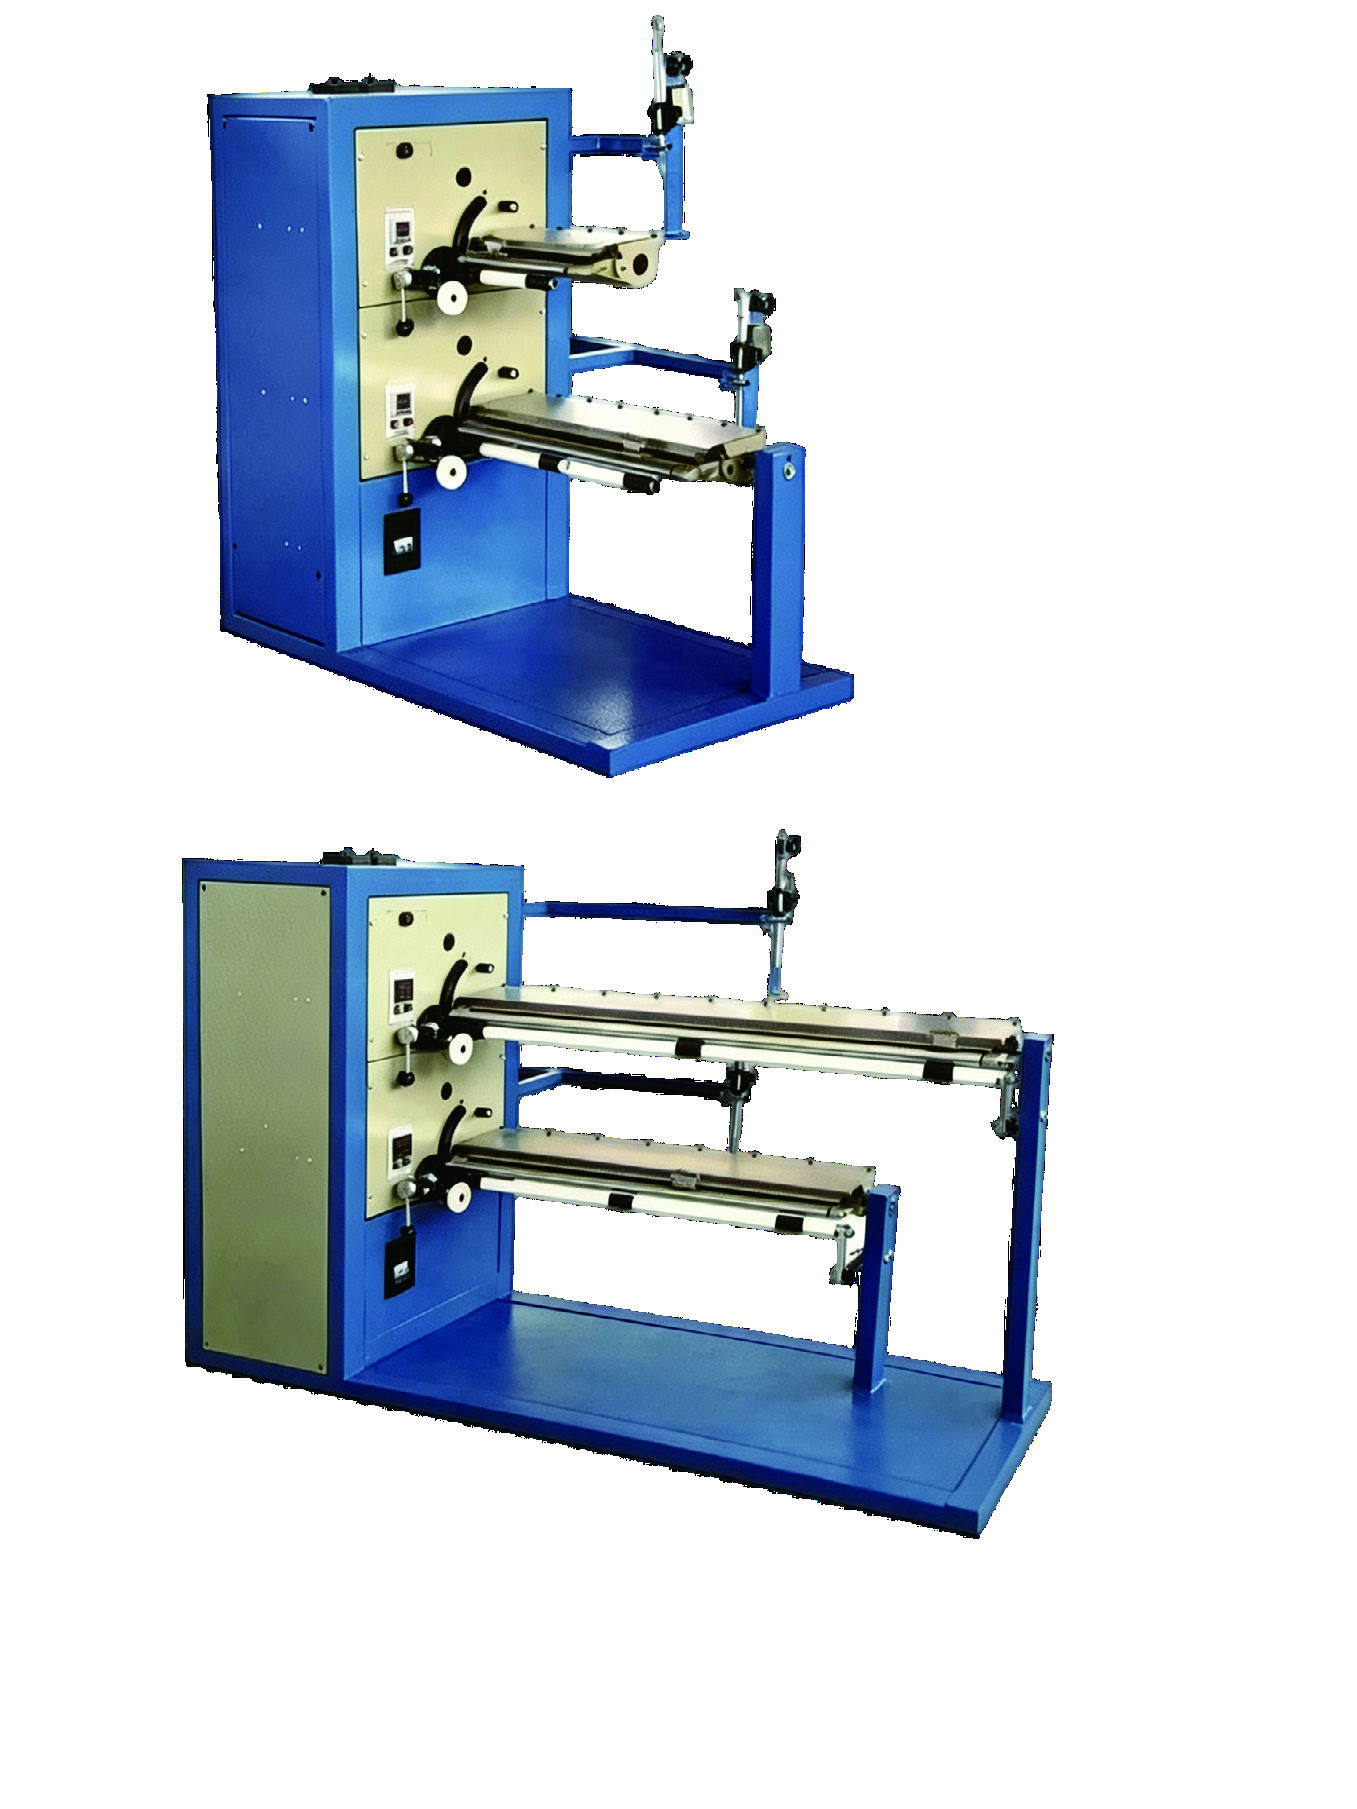
Limited conversions are used deliberately. Drawing, sample or quote using a different basis takes precedence after written technical approval in the project documents.
Filtration Duty
Fluid, particle/challenge, nominal or absolute rating, required flow and differential pressure.
Cartridge Geometry
Length, ID, OD, weight, end-cap/core details, drawing tolerances and allowable changeovers.
Acceptance Basis
Runtime, material lot, good-piece rule, sampled dimensions, defect classification and signed deviation process.
Process Control and Factory Acceptance
A factory acceptance test closes agreed machine requirements with objective records. It is not a substitute for the finished cartridge’s material-safety, structural-integrity, pressure-drop, service-life or contaminant-reduction testing; those proof types are not interchangeable.
Acceptance boundary: IEC 62381:2024 provides a framework for factory and site acceptance testing. Application-specific cartridge performance remains a separate proof obligation.
Freeze the product
Approve the drawing or sample, material, dimensions, weight, rating terminology and finishing state. Unverified claims remain outside the machine acceptance.
Freeze the line scope
List every supplied module, optional station, buyer-supplied interface, utility and safety boundary. Ambiguity becomes a deviation before build.
Freeze the run condition
Agree material lot, settings, net runtime, planned stops, changeover state, operator actions and good-piece definition.
Record the result
Capture total pieces, accepted pieces, rejects by defect, dimensions, weights, faults, stops and corrective action with timestamps.
Review safety and controls
Check guarding, emergency stops, electrical documentation and the installed risk assessment. CTO projects also review dust properties and facility controls.
Close discrepancies
Assign every anomaly an owner, corrective action, re-test rule and signed disposition. A video without traceable conditions does not close acceptance.
A successful machine run does not prove a finished cartridge’s contaminant-reduction claim. The machine FAT verifies conformity to the agreed manufacturing specification; product claims belong to their own application-specific test program.
×
![Enlarged Equipment]()
PRODUCTION LINE
From Cartridge Requirement to Production-Line Handover
The process is built around written decisions. That reduces the risk of a correct machine being supplied for the wrong cartridge, utility, output basis or finishing scope.
Procurement boundary: the NIST equipment pre-purchase guide supports documenting requirements, lifecycle costs and supplier evaluation before purchase.
Requirement brief
The buyer sends cartridge type, material, length, ID/OD, micron terminology, output target, voltage, floor area and destination.
Sample and drawing review
UDMachine checks process family, tooling limits, product variants and which claims require an external test method.
Line configuration
Forming, feeding, cooling, cutting, wrapping, gluing, capping, collection and safety interfaces are marked included, optional or buyer-supplied.
Normalized quotation
The offer aligns scope, utilities, output basis, commercial terms, acceptance criteria, training and spare-parts assumptions.
Build and run-off
Agreed drawings and criteria govern manufacture. The factory run records good pieces, rejects, deviations and closure evidence.
Shipment and support
Packing, shipping documents, installation responsibilities, training format and after-sales boundaries are confirmed in the final contract.
Cases Better Suited to Another Cartridge Process or Line Scope
The right choice is sometimes a different process, a separate finishing module or a test and compliance review before equipment configuration. Forcing every requirement into one machine creates rework, delay and performance risk.
Decision boundary: the U.S. EPA filtration guide supports separating filtration terminology from unsupported performance equivalence.
Do not route yarn-wound media to melt-blown forming.
String wound filter production belongs on a winding process with the correct spindle, traverse, tension and core fixture.
Do not treat carbon block as a PP depth-filter variant.
CTO requires carbon/binder mixing, feeding, extrusion, cooling and cutting, plus a facility review for powder handling.
Do not over-constrain micron rating without the method.
Finer is not always better: it can buy particle retention while costing pressure drop, dirt capacity and usable service life.
Do not use machine output as a drinking-water claim.
RO prefiltration, sediment reduction or drinking water wording requires the applicable finished-product evaluation. The machine specification is not interchangeable with that evidence.
Do not call a forming machine a complete line by default.
If cutting, wrapping, gluing, capping, inspection or collection is required, each station and handoff needs an explicit scope owner.
Do not freeze the quote before the facility boundary.
Voltage, frequency, floor layout, material flow, exhaust, guarding and installation responsibilities can change the configured solution.
Filter Cartridge Equipment Selection Tools
Product-to-Line Fit Screener
Choose the cartridge family, primary material and downstream need. The result is a routing check, not a final machine configuration.
Use ToolPublished Output Basis Normalizer
Put unlike claims onto the same hourly basis. This arithmetic does not predict your machine; it exposes which FAT assumptions still need agreement.
Use ToolComplete-Line Quote Scope Checker
Tick every row that is explicitly included or clearly marked optional in the supplier quote.
Use ToolFactory Acceptance Run Planner
Normalize one observed run into gross rate, accepted rate and yield. The result is evidence for an agreed machine-output condition, not a finished-filter performance certificate.
Use ToolFilter Cartridge Making Machine Questions
Review boundary: answers below separate machine configuration from end-product claims and keep open commercial terms in the quotation. Machinery risk review follows the method described by ISO 12100.
What type of filter cartridge making machine matches PP melt-blown cartridges?
A PP melt blown filter cartridge machine melts and extrudes polypropylene, forms the media on a rotating collection route, cools it and cuts it. Choose 2E&2M or 3E&3M only after the target size, weight, density profile and 24-hour good-piece basis are agreed.
When should a factory choose a string-wound filter cartridge machine?
Choose yarn winding when the product is a string wound filter cartridge built around a PP or stainless core. Yarn, winding pattern, micron grade, core, length and OD must match the intended wound filter cartridges.
What equipment is required for CTO carbon block cartridge production?
The CTO carbon block filter route shown in the supplied brochure includes an automatic mixer, feeder, extruder/workbench, cooling, cutter and dust-collection interface. Downstream wrapping, gluing and capping should be confirmed as separate scope rows.
Is UDF tube extrusion a separate production step?
Yes. The UDF support tube uses PP and master batch on an extrusion line. Customization begins with the tube drawing and tooling; it is not automatically part of a carbon block or finishing machine.
Can one machine make different cartridge lengths and diameters?
Published ranges show possible selection envelopes, not guaranteed one-tool coverage. Send the complete size family so UDMachine can identify tooling changes, setup time, material limits and any incompatible variants.
How do nominal and absolute micron ratings change the brief?
They change the acceptance language. The same micron number can represent different retention behavior, so name the rating basis, particle/challenge method, flow, differential pressure and target result before tying it to a product claim.
What is included in a complete filter cartridge production line?
There is no safe universal definition. Normalize feeding, forming, cooling, cutting, wrapping, heat welding, gluing, capping, collection, inspection, utilities, dust controls, FAT, training and spares as included, optional or buyer-supplied.
How should buyers compare rated power with actual running power?
Rated power supports the electrical design; running power describes a stated operating condition. Confirm both, plus voltage, frequency, peak/start behavior and which modules were active during the running-power observation.
What verifies production capacity and finished-cartridge performance?
Production capacity needs an agreed run condition and good-piece record. Finished-cartridge performance needs the appropriate material, structural, pressure-drop, dirt-capacity, service-life or contaminant/challenge testing. One does not replace the other.
What affects filter cartridge machine price and lead time?
Process type, capacity configuration, extruders/spindles, tooling, size changes, automation, finishing, voltage, safety interfaces, FAT, training, spares and shipping scope drive price. Production schedule, MOQ and payment milestones should be confirmed in the configured quotation; no UDMachine-specific terms were supplied for this page.
What should a factory acceptance test include?
Include the approved product basis, machine configuration, material, settings, net runtime, good-piece rule, measurements, rejects, stops, safety checks, deviation log, corrective action, re-test and sign-off.
What training, spare-parts and after-sales evidence should buyers request?
Request named training format and duration, installation responsibilities, manual/electrical documents, recommended commissioning and wear spares, response channel, warranty boundary and escalation route. Put the agreed support terms in the final quotation or contract.