Get in touch with Suzhou UDTECH Technology Co., Ltd. Company

UDF Tube Making Machine for Plastic Filter Cartridge Tubes
A UDF tube making machine should be configured around the tube you need, the way that tube will be measured, and the equipment connected before and after it. Send the finished-tube requirements first so the proposal can map the extrusion line boundary without confusing it with carbon filling or end-cap assembly.
UDF Tube-Line Scope Split
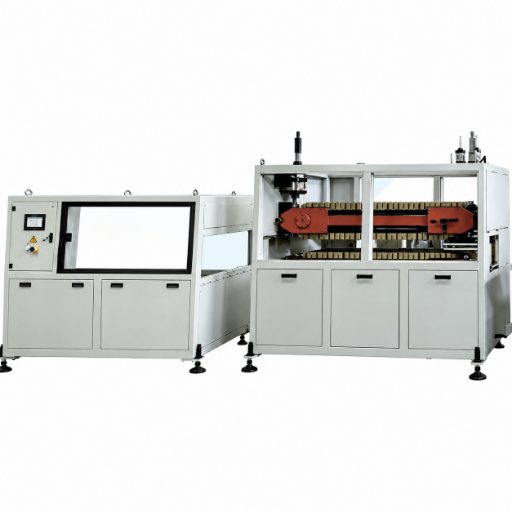
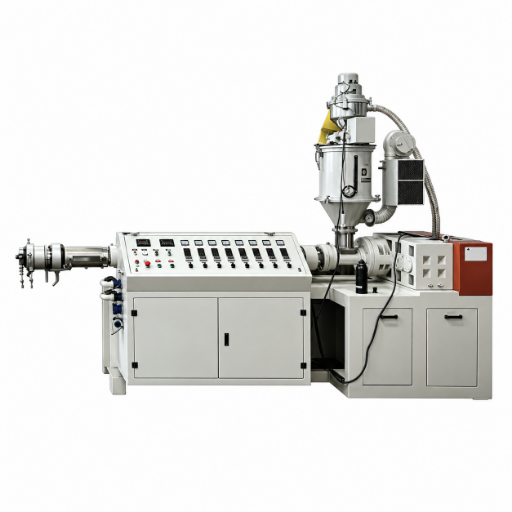
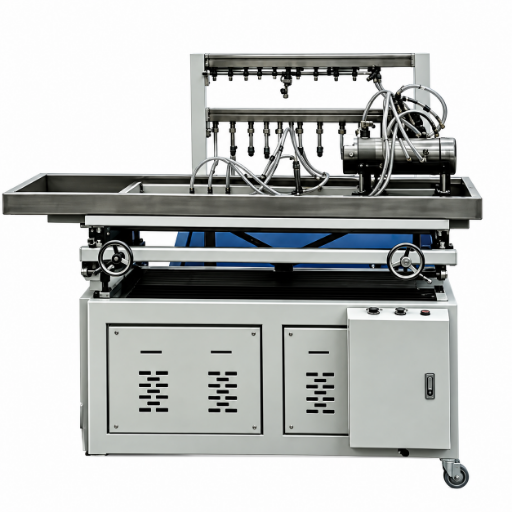
The three equipment routes may share a filter-cartridge project, but serve different functions. Begin with the component, then verify which production line owns that component as its output.
These routes are not interchangeable. Unlike a single brochure label, this split exposes the handoff; the mistake is to compare prices before confirming which component and process each quotation includes.
INPUT
documented plastic material or formulation plus the finished-tube specification.
- Material feed and melt process
- Tube form, calibration, and cooling
- Haul-off, cutting, collection, or downstream handoff
OUTPUT
a tube prepared for the agreed next operation.
INPUT
housings or tube components, carbon media, separators, and end caps.
- Media filling or dosing
- Component positioning
- Cap joining and cartridge handling
OUTPUT
an assembled cartridge, subject to its own quality plan.
INPUT
the specified carbon blend and binder system for a separate forming process.
- Material preparation
- Carbon-block forming
- Cooling, cutting, and later assembly
OUTPUT
a formed carbon block, not a UDF plastic tube.
The practical benefit of the split
Your quotation can state which line owns tube production, which unit performs optional downstream work, and which assembly equipment belongs in another proposal. This prevents a low headline price from hiding a missing station or an assumed handoff.
Plastic Tube Extrusion Stages for Engineering Review
Treating the UDF plastic tube production line as a matched system helps explain why die gap and drawdown, cooling, and pipe extrusion tooling must be reviewed together.
The risk of reviewing the extruder alone is a line mismatch because die, cooling, haul-off, cutting, and measurement interact. The proposal should be engineered around the finished-tube brief and the agreed line boundary; the official page for ISO 3126:2005 and trade-press extrusion guidance provide measurement and process background, not a claim of certified machine performance.
The trade-off to record
A larger isolated output claim does not resolve cooling stability, dimensional acceptance, cutter coordination, or the downstream handoff. Compare the complete agreed condition and the accepted-product definition.
01
Material Feed and Melt Process
The review starts with resin identity, formulation, colour, regrind restriction, moisture or conditioning requirement, and the intended water-filter application. A generic material name is not a process setting, so the exact grade or a representative sample belongs in the enquiry.
02
Die, Mandrel, and Tube Form
Outer diameter, inner diameter, wall target, and the permitted variation guide the tooling discussion. Finished dimensions also depend on material response, temperature, drawdown, centring, and the operating condition rather than nominal die geometry alone.
03
Calibration and Cooling
The calibration method and cooling path must stabilise the tube without building avoidable distortion into it. Tank length, water condition, line speed, and the product cross-section should be reviewed together.
04
Haul-Off and Cutting
Pulling speed influences drawdown and must coordinate with the cutter or collection unit. Cut length, end condition, dust or chip control, and the next handling step belong in the same boundary review.
05
Inspection and Handoff
Define where samples are taken, which dimensions are measured, how acceptable product is counted, and who releases the trial. If perforation, slotting, filling, cap assembly, or packaging follows, record whether it is included, optional, buyer-supplied, or outside the tube line.
Tube Materials and Finished-Tube Inputs
Material review applies to a documented grade and application, not to a blanket guarantee that every polypropylene (PP) or plastic pipe blend will perform the same. The wrong grade can shift melt response, cooling, and trial results, while a polymer family label does not replace an exact grade and formulation.
| Buyer input | Why engineering needs it | Evidence to send |
|---|---|---|
| Resin and exact grade | Separates material identity from a generic polymer label | Supplier data sheet and grade designation |
| Formulation and additives | Colourants, fillers, stabilisers, and other modifiers can change flow and cooling behaviour | Formulation note or compound data sheet |
| Regrind or recycled-content rule | Defines whether reprocessed material is prohibited, capped, or trialled separately | Written limit and lot-control method |
| Tube function | Connects geometry to support, flow, fit, and downstream assembly requirements | Cartridge drawing, sample, or interface sketch |
| Water-contact basis | Identifies the product or market requirement the buyer must satisfy | Applicable specification or customer requirement |
| Representative trial material | Lets the trial use the intended grade instead of an unrelated substitute | Agreed quantity, batch identification, and shipping condition |
Changeover and Downstream Interfaces
A diameter change can require different tooling and calibration adjustments, while a length change belongs to the cutting cycle. ISO 3126 provides relevant dimensional-measurement background; a perforation-pattern change may belong to an optional downstream process rather than the extrusion machine.
| Requirement | Engineering review | Line boundary |
|---|---|---|
| Outer or inner diameter change | Tooling, centring, calibration, cooling, and restart evidence | Core extrusion configuration |
| Wall-thickness change | Material flow, die setting, drawdown, measurement frequency | Both parties freeze the acceptance method |
| Cut-length change | Haul-off coordination, cutter cycle, end quality, collection | Supplier states the included cutter and range after review |
| Perforation or slotting | Pattern, pitch, open area, burr condition, chip control | Proposal states included, optional, or excluded |
| Carbon filling and end caps | Dosing, positioning, joining, and complete-cartridge handling | Separate UDF assembly route |
| Downstream transfer | Tube orientation, buffer, collection, interface height, controls | Interface owner named in writing |
Twelve Inputs That Configure the Line
12-Input Tube Specification Card
The fastest path to a useful UDF tube making machine proposal is a finished-tube brief that the engineer can test for completeness. Use the same product definition when comparing suppliers, because a different material, diameter, acceptable-product rule, or operating period produces a different answer.
| # | Input | Unit or format | Why it changes the review | Freeze point |
|---|---|---|---|---|
| 01 | Tube application | Cartridge position and function | Defines support, flow, fit, and contact-water questions | Before configuration |
| 02 | Material or formulation | Exact grade and data sheet | Changes melt, die, cooling, and trial decisions | Before tooling review |
| 03 | Outer diameter | mm or in plus tolerance | Sets tooling, calibration, and measurement needs | Technical agreement |
| 04 | Inner diameter | mm or in plus tolerance | Connects bore, wall, flow, and mating-part fit | Technical agreement |
| 05 | Wall thickness | Nominal value and permitted variation | Links material flow, drawdown, cooling, and product mass | Technical agreement |
| 06 | Cut length | mm or in plus tolerance | Defines cutter cycle and downstream collection | Before trial |
| 07 | Measurement method | Locations, instrument type, condition, precision | Makes supplier and buyer results comparable | Acceptance plan |
| 08 | Perforation or post-process | Drawing, pitch, pattern, open area, burr rule | Determines whether another unit or process is required | Line boundary |
| 09 | Target output and basis | Accepted tubes, length, mass, or another named unit per period | Prevents headline production figures from using different denominators | Quotation |
| 10 | Electrical supply and utilities | Voltage, frequency, phases, water, air, ambient condition | Connects the machine to the destination factory | Quotation and site plan |
| 11 | Available space | Length, width, height, access, service clearance | Tests whether the complete line and maintenance access fit | Layout approval |
| 12 | Downstream interface | Manual collection, buffer, transfer, or assembly input | Assigns the physical and control handoff | Scope release |
Dimensional acceptance
A standard measurement plan should cover the dimensions that matter to the component, such as outer diameter, inner diameter or wall, length, straightness or ovality where relevant, end condition, and any perforation feature. ISO 3126 and the trade-press discussion of closed-loop tube dimension control provide useful background, while your product drawing remains the purchase requirement.
Quotation Scope and Commercial Inputs
Price depends on purchased line configuration, tooling, controls, downstream cutting or post-processing, site conditions, scope of trial and acceptance, service package, destination, and documentation. A written quotation makes clear what is included and optional, what needs to be supplied by the customer, and what is not included.
- Main extrusion machinery and controls
- Die, mandrel, calibration, and change parts
- Cooling, haul-off, cutting, collection, and options
- Guarding and interface responsibility
- Trial material, sample, and acceptance records
- Installation, commissioning, training, and travel
- Utilities, layout, lifting, foundations, and local labour
- Spare parts, document language, remote support, and onsite service
What the quotation should confirm
Price basis
Currency, validity, tax or duty boundary, and each included module
Order quantity
Minimum order or package rule stated for this proposal
Production schedule
Start condition, approval milestones, and shipment readiness definition
Payment
Stages, documents required for each stage, and bank method
Delivery term
Named Incoterm, named place, packaging, freight, insurance, and import responsibility
Warranty and remedy
Coverage, exclusions, response route, spare-part responsibility, and remedy process
Acceptance, Measurement, and Machine-Safety Inspection
Acceptance should move from a tube specification to an observed record. Both parties should agree upon the sample, variables, measurement method, an acceptable criterion, record owner, and release point before a factory trial begins.
Changeover, Safety and Acceptance Evidence Ladder
Compare the line by the accepted tube it produces under the agreed condition—not by the largest isolated number in a brochure.
-
Evidence level1. Buyer definitionAgreed variableDrawing, sample, material, application, utilities, and downstream interfaceRecord ownerBuyer project ownerRelease pointEngineering review can begin
-
Evidence level2. Configuration recordAgreed variableLine modules, tooling, controls, safety interfaces, options, and open itemsRecord ownerSupplier engineerRelease pointQuotation and technical agreement
-
Evidence level3. Trial and measurement recordAgreed variableMaterial batch, settings, run condition, samples, dimensions, defects, and accepted-product countRecord ownerNamed trial and quality ownersRelease pointFactory acceptance decision
-
Evidence level4. Handover recordAgreed variableDocuments, spares, training scope, site actions, commissioning checks, and unresolved itemsRecord ownerJoint project teamRelease pointShipment or site-stage release
-
Access and Heat
Review material-feed access, screw and drive access, hot surfaces, die work, and molten-material exposure during operation, shutdown, and cleaning.
-
Movement and Cutting
Review haul-off nip points, rotating parts, cutter access, ejected material, collection, and the behaviour of each station during a stop.
-
Risk Reduction
Define guards, interlocks, emergency stops, isolation, restart control, signage, and integration responsibility for the actual layout.
How We Work: From Tube Specification to Line Handover
A unacknowledged responsibility gap can hinder approval of a quotation, trial record, and site layout if each document applies its own assumptions. In contrast, this sequence assigns each open item to a document, owner, and release point.
Open-item discipline
An open field should have an owner and a date or project milestone for resolution. That is more useful than allowing a blank cell to become an assumption after the equipment is built.
Specify the finished tube.
Provide the application, material, drawing or representative sample, dimensions, permitted variation, downstream processing, and subsequent fit.
Ensure all twelve inputs are checked.
Include the target output basis, electrical supply, utilities, available space, and handoff to the next stage.
Outline the process flow and options.
The engineering review distinguishes core extrusion, tooling, cooling, haul-off, cutting, optional downstream processes, and customer-provided infrastructure.
Verify the scope outlined in the written proposal.
The proposal records included equipment, unresolved technical issues, commercial details, site work, documentation, service plans, and division of responsibilities.
Design the trial and acceptance plan.
Both parties agree on materials, samples, testing conditions, measurement method, acceptance criteria, documentation, and authority to release.
Prepare the site and handover.
Layout, utilities, access, local safety work, installation, commissioning, training, spare parts, and support are confirmed against the written quotation.
UDTECH Manufacturing, Inspection, and Support Basis
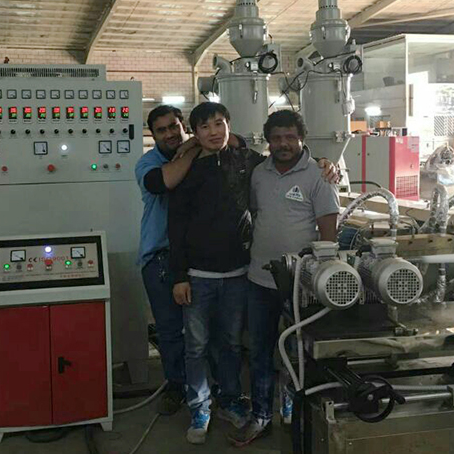
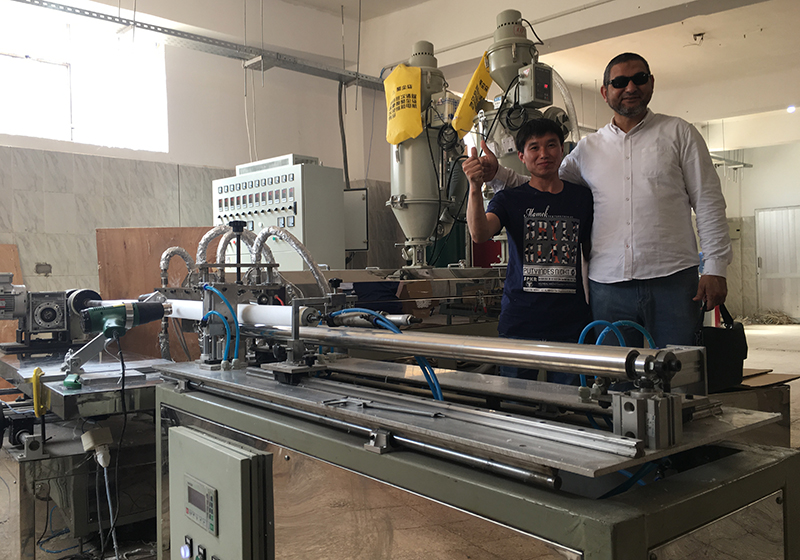
Suzhou UDTECH Technology Co., Ltd. independently develops and manufactures filtration equipment, serves the domestic market, supports global exports, and provides technical after-sales service. These are company-level capabilities; the tube line itself is configured and released against the written project scope.
6,000 m²
Standardized Workshop
Our company operates a 6,000-square-meter standardized workshop for its manufacturing activities.
55+ countries
Company Export Reach
Our equipment portfolio has been exported to more than 55 countries. That company statement is not presented as a UDF tube-line installation count.
Research and Production
We keep independent research, product development, and equipment production within the UDTECH company scope.
Manufacturing Resources
Our company maintains manufacturing equipment for its filtration-machinery production work.
Laboratory and Testing Resources
Our company maintains laboratory and testing equipment and applies quality control through the production process.
Technical Support
We provide technical after-sales support at company level. The proposal should state the service channel, language, remote or onsite boundary, and any chargeable work for this project.
Engineering Assessment Tools
Frequently Asked Questions: UDF Tube Making Machine
What does a UDF tube making machine produce?
It is scoped to produce the agreed plastic tube component for a UDF/GAC water-filter cartridge. Carbon filling, end-cap assembly, complete-cartridge testing, and finished-filter performance belong to separate operations unless the quotation adds them.
What is the difference between a UDF tube line and a UDF cartridge assembly machine?
The tube line forms and cuts the plastic tube from the agreed material. An assembly machine starts with prepared components and may fill media, position separators or caps, join parts, and handle a completed cartridge.
Which 12 inputs are needed to configure the line?
Send the tube application, material or formulation, outer diameter, inner diameter, wall thickness, cut length, measurement method, perforation or post-process need, target output basis, electrical supply and utilities, available space, and downstream interface.
How are tube diameter, wall thickness, and length changes reviewed?
Engineering checks tooling, calibration, cooling, haul-off, cutting, change parts, restart method, and the sample measurement plan. The proposal should state which changes are covered by the base line and which need another part or module.
Which material information and samples should a buyer provide?
Provide the exact grade, data sheet, formulation or additives, colour, regrind rule, intended use, and any water-contact requirement. A representative material batch and tube or cartridge sample make the trial plan more specific.
How should output be compared between suppliers?
Use the same tube dimensions, material, acceptable-product definition, output unit, operating period, changeover and stop treatment, scrap treatment, and downstream boundary. A line-speed or mass figure without that denominator is not a direct comparison.
Which utilities, voltage, and factory-space inputs are required?
State voltage, frequency, phases, available power, process water, cooling-water condition, compressed air, ambient condition, floor dimensions, access, service clearance, drainage, lifting, and the next machine interface. The written layout should assign infrastructure and connection work.
How are trial material, measurements, and acceptance records defined?
The plan names the material batch, sample geometry, operating condition, measurement locations, instrument method, permitted result, sample count, acceptable-product rule, record owner, and release authority. Safety inspection and open items should appear in the same acceptance pack.
Which commercial details must the written quotation confirm?
Confirm price basis, minimum order or package rule, schedule milestones, payment stages, named Incoterm and place, warranty and remedy, packaging, freight boundary, installation, commissioning, training, travel, spares, document language, and service scope.
What does the written quotation confirm about scope and support?
It should separate included equipment, options, buyer-supplied items, exclusions, site work, interfaces, trial and acceptance work, handover documents, remote support, onsite service, and unresolved questions. Ask for every open item to have a named owner and closure point.