Get in touch with Suzhou UDTECH Technology Co., Ltd. Company

Filter Cartridge Making Machines
Quote in 24 hours
Minimum order 1 set
1–100 micron on cartridges up to 1016 mm
UDTECH designs three filter cartridge making machines: a PP melt blown line, string wound winder, and CTO activated carbon extrusion line. While each line makes a different cartridge, it is worth noting that different variables hold each rating, and that they play a different role in the downtime spent to change them.
- The specification envelope for all three line families, shown side by side in one table.
- What moves the price, what the payment terms are, and what a quotation covers.
- The two purchases first-time buyers almost always get in the wrong order.
Request a quotation
Send a drawing, a photo or a written specification. Whatever you already have is enough to start a configuration.
Quote turnaround
Within 24 hours, from someone who has read your specification
Minimum order
1 set. We build and ship single lines
Filtration accuracy
1–100 micron across the melt blown and
SYS_MOD // 01
01
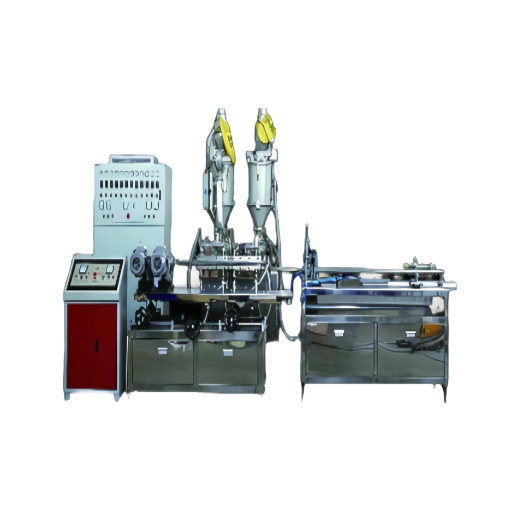
PP melt blown line
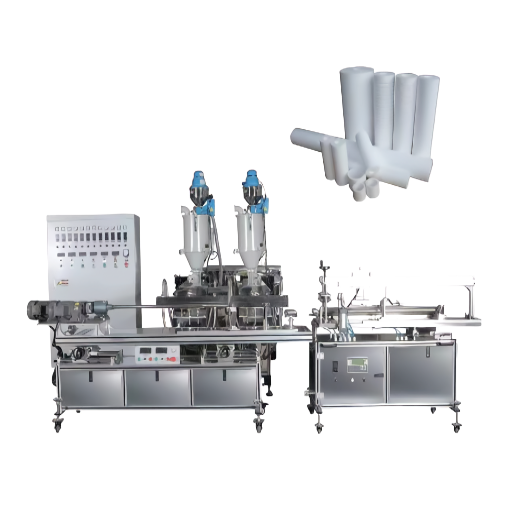
Using a single pass, polypropylene granules go in and finished depth cartridges come out through these stages: extrusion, fiber placement on a rotary mandrel using hot air to thin the fiber, and cutting. The line uses a fully automatic control system with no yarn, no adhesive, and no core.
- Best for sediment and general depth filtration sold in volume, where the cartridges have graded density through the wall.
- This is also known as a PP spun filter cartridge machine in India and the Middle East. Same process, same machine, different market terminology.
- Watch the cartridge weight behind any published piece count.
- Sold into water purification pre-treatment, circulating cooling water, boiler water and general water treatment, plus pharmaceutical, electroplating and beverage.
SYS_MOD // 02
02
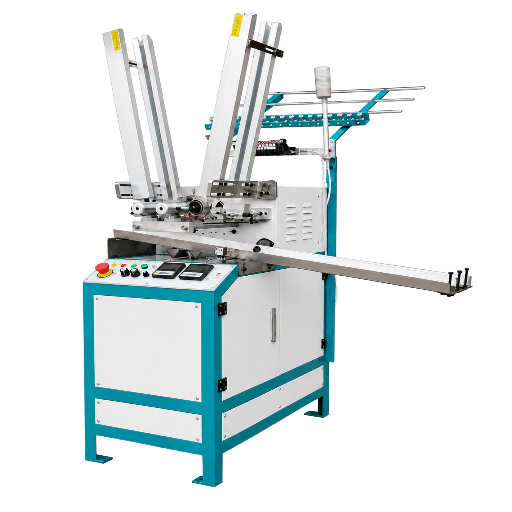
String wound winder
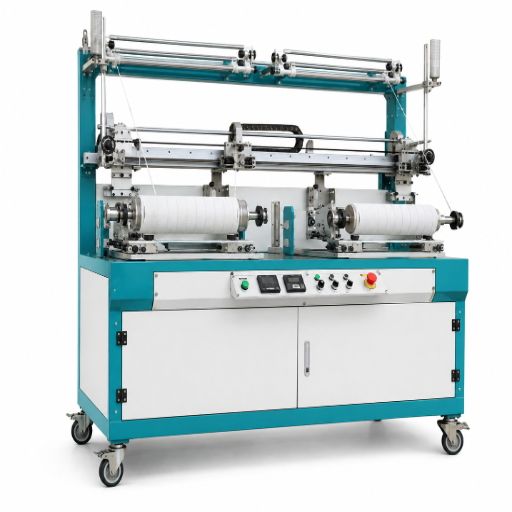
Textile fibre yarn is wound onto a porous core under controlled tension and traverse. The yarn winding machine runs at 60–320 m/min and takes PP or stainless steel cores.
- Ideal for high dirt-holding jobs and larger particle bands. Also used in shops that prefer to change rating by changing yarn as opposed to changing the process recipe.
- Cores come off of a separate extrusion line which is the machine that most first-time buyers do not factor into the cost.
- View the yarn specification. It carries more of the result than the machine does.
- Sold into reverse osmosis (RO) pre-treatment and general water filtration.
SYS_MOD // 03
03
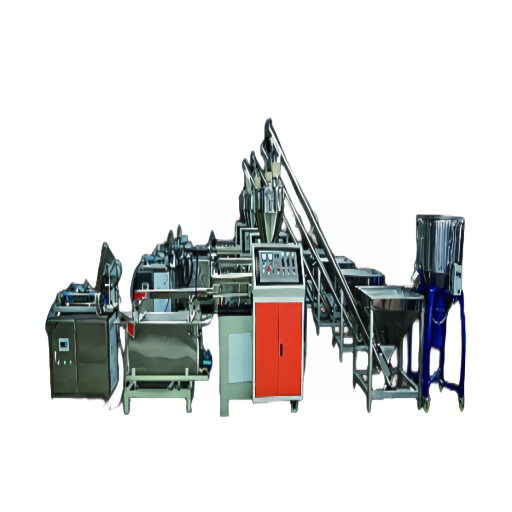
CTO carbon block line
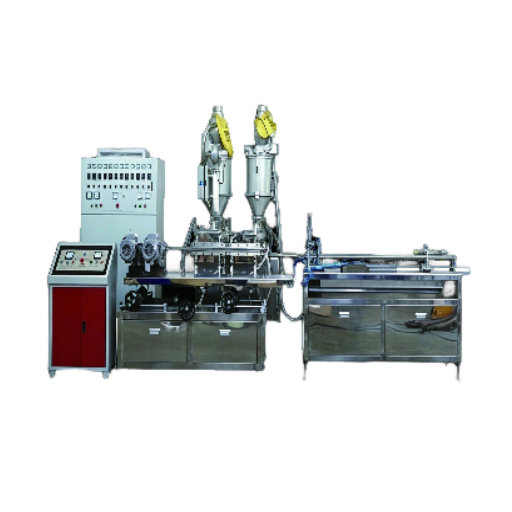
Activated carbon granule and PE powder are mixed, fed, extruded through a heated barrel, cooled, cut and dust-extracted. The line runs 24 hours without a break and produces one 10 inch cartridge every 50–60 seconds.
- Best for chlorine removal, taste and odor removal in point-of-use and point-of-entry cartridges.
- Constraint: one extruder produces one combination of inner and outer diameter, and changing it requires barrel and screw changes.
- Notice the dust. The line has a collector for a reason.
- Sold into point-of-use and point-of-entry water filtration, where an activated carbon block cartridge removes chlorine, taste and odor.
What buyers call these machines
Search vocabulary fluctuates from market to market. A filter making machine, a filter machine, a filter cartridge machine or a spun filter manufacturing machine all refer to the same three lines. In India and the Gulf, similar equipment is searched as a pp filter making machine, a spun filter making machine or an RO spun filter manufacturing machine, because most of these cartridges end up in reverse osmosis (RO) pre-treatment. As a filter cartridge machine manufacturer we quote them the same, regardless of the name you end up with.
The Chain Before the Cartridge
A cartridge plant is not a machine. Five classes of machines fill the gap between a lump of polymer and a boxed cartridge, and every competitor page in this category sells exactly one.
| Stage | Equipment class | What it decides |
|---|---|---|
| 1. Core | PP tube extrusion line | Whether you buy cores or make them, and the bore every wound cartridge is built on |
| 2. Forming | Melt blown line, wound winder or carbon extruder | The medium, the micron band and the output rate |
| 3. End caps | Gluing and capping machine | Which housings your cartridge fits. See The Second Machine Question below |
| 4. Wrapping | Carbon block filter wrapping machine | The non-woven outer layer on carbon cartridges |
| 5. Inspection | Test rig and packing | Whether batch ten matches batch one |
UDTECH produces machines for stages one to four. The Chain Before the Cartridge explains why a quote for a cartridge plant is not equivalent to a single machine price, and why we ask you what you’re planning to sell before we ask which machine you’re interested in.
Ancillary machines that finish the cartridge
UDF tube making machine
for PP cores and profiles: 20 kW per set rated, 10 kW/h running, footprint 1.5 m by 13.5 m, and a minimum of 30 square meters of floor area.
Full-automatic gluing and capping machine
for carbon rods: AC 220 V / 50 Hz, 2000 W, PLC and HMI control, automatic ejection, non-woven wrapping, heat welding, automatic discharge.
Filter wrapping machine units
Full-automatic carbon block filter wrapping machine units and semi-automatic gluing and capping machine units for slower throughput lines.
Not sure which line fits what you sell?
Answer four questions and get a shortlist
Start the Line SelectorCartridge Output Formats and End-Cap Welding Scope
Knowing where the forming line stops and a separate finishing machine starts is the most useful piece of information on this page.
The Second Machine Question
Everyone knows which machine is the first one to buy. The Second Machine Question, however, is usually not about buying another forming line.
The wound and melt blown lines we manufacture ship with the ability to produce double open ended cartridges.
Every 222, 226, fin and single open end configuration is added by a separate end-cap and adapter welding operation, which is its own machine class and its own line on the quotation.
The Second Machine Question is answered by your customers’ housings, not by which medium sells the most.
If your customers purchase 222 and 226 fittings, your second machine is a capping machine, and the forming line you purchased as the first part of the plant is half of the plant.
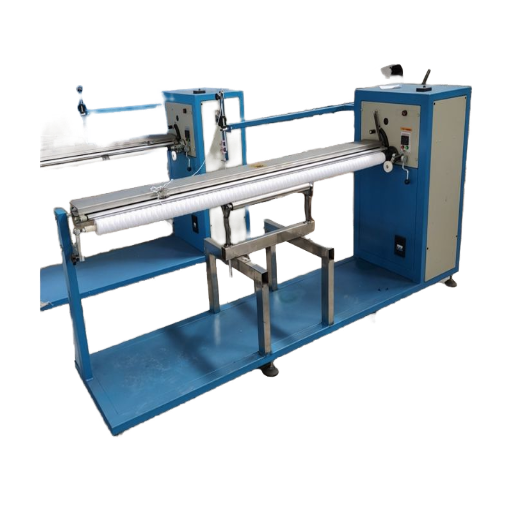
End-cap routes and where each one sits
Adhesive bonding
How it works
Cap bonded to the cartridge face with a curing adhesive
Where it sits
Separate station
Heat and fusion welding
How it works
Cap and cartridge face melted together, no adhesive
Where it sits
Separate machine. This is the route our gluing and capping machine uses
Spin welding
How it works
Friction weld. A Pall Corporation patent works the example at 500 to 4,000 rpm, preferably 1,725 rpm, holding contact for 20 to 35 revolutions at an initial pressure of 50 to 90 psi[7]
Where it sits
Separate machine
Integral molding
How it works
Cartridge end embedded into thermoplastic melted against a heated die. Both caps can be formed at once, and a connector or adapter can be incorporated in the same step[8]
Where it sits
A different process route, patented for pleated and wound media
We build the heat-welding route: a full-automatic gluing and capping machine at AC 220 V / 50 Hz and 2000 W with PLC and HMI control. It is quoted as its own scope rather than bundled into the forming line, so you can see what you are paying for.
DATA_LINK // SPECIFICATIONS
Specification Envelope Across the Three Lines
Every figure shown below comes directly from UDTECH for their machines. The table applies to the same machines whether your market calls them melt blown lines or spun filter manufacturing machines.
| Specification | PP melt blown | String wound | CTO carbon block |
|---|---|---|---|
| Filtration accuracy | 1, 5, 10, 20, 30, 50 up to 100 micron | 1, 5, 10, 20, 50, 100 micron | Set by carbon grade and binder ratio |
| Default inner diameter | 28 mm (1.10 in) | 28 mm (1.10 in) | 38 mm (1.50 in) |
| Inner diameter range | 10–150 mm (0.39–5.91 in) with a matched mandrel shaft | 28 mm standard, other bores on request | 9–100 mm (0.35–3.94 in) |
| Outer diameter | 38–120 mm (1.50–4.72 in) at 28 mm bore | 29–150 mm (1.14–5.91 in) | 63 mm default, 29–150 mm (1.14–5.91 in) range |
| Cartridge length | 254 / 508 / 762 / 1016 mm (10 / 20 / 30 / 40 in) | 254 to 1016 mm standard (10 to 40 in), longer to order | 127 / 254 / 508 / 762 mm (5 / 10 / 20 / 30 in) |
| Cartridge weight | 70–200 g (2.5–7.1 oz), adjustable | Set by yarn and layer count | Set by wall thickness |
| Output | 3,500–4,200 pcs / 24 h on 2E&2M, 5,000–5,800 on 3E&3M | 60–320 m/min winding speed | One 10 inch cartridge every 50–60 seconds |
| Connected power | 70 kW on 2E&2M, 100 kW on 3E&3M | 0.18 kW at 10 in to 0.55 kW at 40 in | 16.45 kW per set |
| Running power | 28–32 kW/h on 2E&2M, 38–40 kW/h on 3E&3M | Motor rated as above | 8 kW/h when running |
| Supply voltage | AC 380 V / 50 Hz or 220 V / 50 Hz | AC 380 V / 50 Hz, other voltages configurable | AC 380 V / 50 Hz |
| Duty cycle | Continuous | Continuous, automatic stop when the yarn package is full | Runs 24 hours without a break |
| Feedstock | Polypropylene granules | PP yarn, PP or stainless steel core | Activated carbon granule and PE powder |
| Core material | Coreless | PP core, stainless steel core, others on request | Coreless |
| Cam material | Not applicable | Polyoxymethylene | Not applicable |
INFO: Inch conversions use the exact definition of the inch as 25.4 mm, fixed by Federal Register notice 59-5442.
ACTION_BAY // DEPLOY
Measure your line before you request pricing.
Enter in the cartridge weight and length you would sell and the output shown above convert into the amount you would actually get.
Pricing Mechanism, Lead Time and Payment Terms
A filter cartridge making machine price is not a list number, it is an output of the configuration. Prices for this equipment class in platforms range from around USD 20,000 to USD 50,000 per machine, and that range is configuration, not negotiation.
Where a first plant usually starts
If you are sizing a small filter cartridge making machine for a first plant, the entry melt blown line at 3,500–4,200 pieces per 24 h is where most producers start, because it covers the widest cartridge market with one set of tooling. Five decisions move the number from there.
Throughput tier
Two extruder and die sets or three on the melt blown line, which would move the base cost and connected load from 70 kW to 100 kW.
Dimensional range
Bores outside the 28 mm default would need a matched mandrel shaft, and lengths outside the standard set would need tooling.
Automation scope
Servo cutting and winding stations, and any end-cap and adapter welding, are separate line items rather than parts of the forming line.
Electrical package
Matching your local grid is standard. Anything outside 380 V / 50 Hz or 220 V / 50 Hz is a quotation line item.
Documentation package
Export documentation and factory inspection support are quoted with the order.
Terms
Detailed conditions for production.
30% T/T deposit releases the build slot, with the balance settled before shipment. Letters of credit are accepted.
1 set. We build and ship single lines.
The string wound winder is scheduled at 30 working days. Melt blown and carbon block lines are quoted against specification.
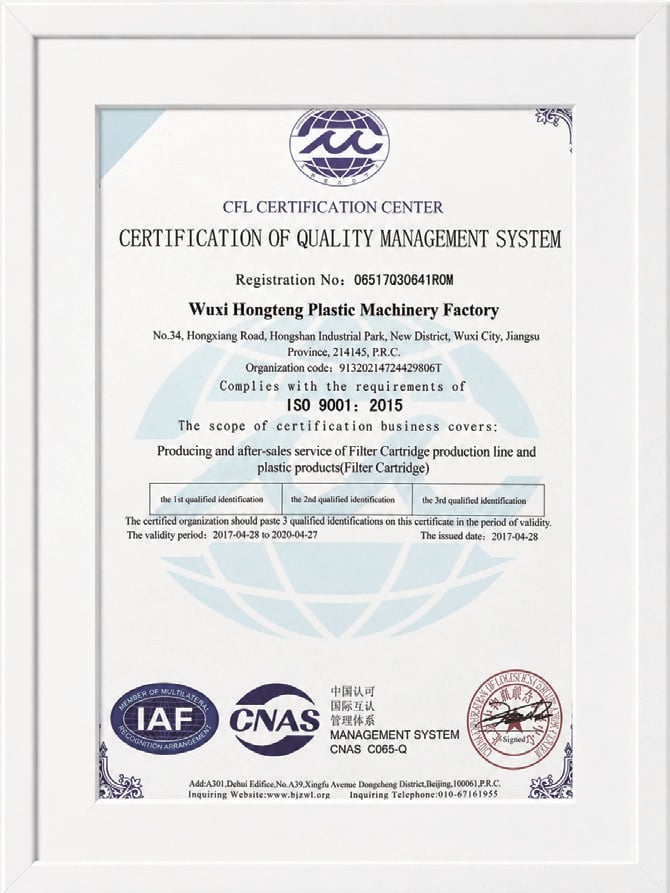
12-month warranty from delivery.
Energy per line, on its own declared basis
Below is what each line draws and what it produces. Read each row on its own, because the three lines make different cartridges and ranking them against each other on kilowatt-hours would compare three different products.
Hover mouse to reveal data table ➔Energy Specifications Overview
| Line | Connected | Running | Published output, and its basis |
|---|---|---|---|
| Melt blown 2E&2M | 70 kW | 28–32 kW/h | 3,500–4,200 pcs / 24 h. Cartridge weight is adjustable across 70–200 g, ask us to restate. |
| Melt blown 3E&3M | 100 kW | 38–40 kW/h | 5,000–5,800 pcs / 24 h at the same open basis |
| String wound | 0.18–0.55 kW | Motor rated | 60–320 m/min of yarn. Pieces per shift depend on cartridge length and layer count. |
| CTO carbon block | 16.45 kW / set | 8 kW/h | One 10 inch cartridge every 50–60 seconds, continuous |
Two comparisons in that table are like for like
- Our melt blown line draws 28–32 kW/h against a published competitor figure of 30–35 kWh on a 65 kW machine of the same type.
- Another listed melt blown line that has a comparable output of 3,200–4,200 pieces per day uses 37 kW per hour.
Knowing the energy consumption is important, but it won’t be the decider here. In a cartridge plant’s cost base, utilities occupy a single digit percentage, whereas the raw material cost is the major contributor. This means the carbon and the resin you source locally will impact your margin more than the motor rating.
Factory Run-Off, Documentation and Warranty
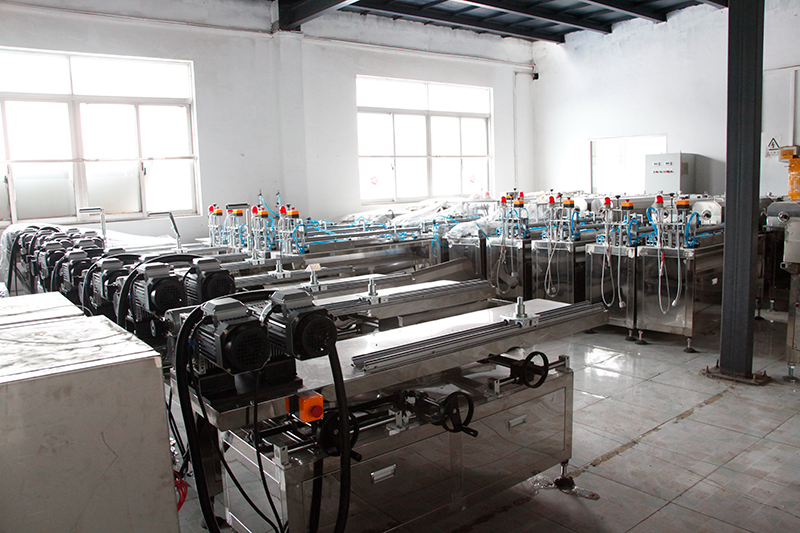
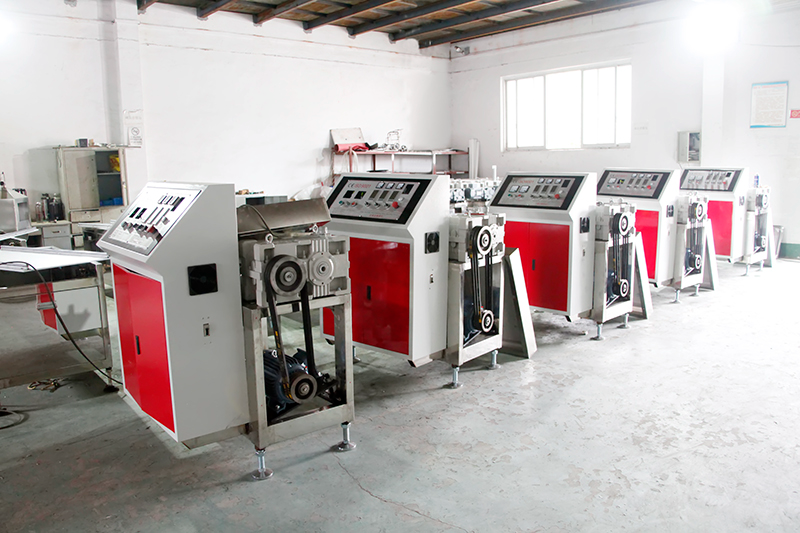
Every line is assembled and test-run at our factory before it ships. That run is where the recipe for your cartridge specification is proved, and it is the only point at which a defect can still be corrected by the people who built the machine.
What ships and what we commit to
- An operation manual and a commissioning video ship with the line.
- Inspection support and the support for the preparation of export documents are included in the quoted price.
- Installation assistance, startup and commissioning support, and technical support for the automatic control system, with a direct line to technical service for overseas customers.
- 12-month warranty from delivery.
The interval that decides batch ten
The risk on these processes is never the first batch because the die and spinneret passages that hold your rating narrow as the polymer degrades against the hot metal. Talk to some experienced melt blow producers and they will tell you that the hardest part of the job is product stability, not capacity.
A line that passes its factory run can deteriorate within weeks if cleaning is neglected, which is the trade-off for every unattended-running claim in this category.
On the carbon line the equivalent is binder build-up in the barrel.
Plan the spares position at the order stage. Buyers negotiate hard on price and rarely think about the morning two years out when the machine stops working, and by then spare-part lead times run into weeks while an idle line costs far more than the part.
This is a live research problem rather than a settled one. The published continuous melt blown apparatus cited above introduces a control and interface layer to add overall equipment effectiveness, total effective equipment performance, loading time, utilization, performance and yield.[5]
Machine safety scope, settled at quotation
Guarding, interlocks, emergency stop circuits, anchoring and positioning requirements should be on the proposal and not discussed after delivery. Two other tasks are now yours as the employer.
- 29 CFR 1910.212 covers general machine guarding for rotating parts and nip points, which every winder and every extruder has.[4]
- 29 CFR 1910.147 discusses control of hazardous energy and the lockout and tagout procedure for the die head and barrel that your maintenance team will be required to perform.
- Electrical approval. 29 CFR 1910.303(a) requires workplace electrical equipment to be approved, and 29 CFR 1910.399 resolves that to acceptance by a nationally recognized testing laboratory.[1] A CE mark is a European instrument and does not satisfy it.
- NFPA 79 pertains to the electrical equipment of industrial machinery and NEC Article 409 requires an industrial control panel to carry a short-circuit current rating on its label.
Certifying the cartridges your line makes
This is the point that is most frequently mis-sold in this category, so here it is simply. Certification applies to the complete cartridge and the system it is in, not to the machine, and no machine can transmit its status to the cartridges it produces.
| Standard | Scope | What gets tested |
|---|---|---|
| NSF/ANSI 42 | Aesthetic effects: chlorine, taste and odor, chloramine, particulate, iron, manganese, zinc, total dissolved solids | Material safety including content to NSF/ANSI/CAN 372, structural integrity, and the specific reduction claims made[2] |
| NSF/ANSI 53 | Health effects: over 50 reduction claims including lead, Cryptosporidium, volatile organic compounds and chromium | The same three-part structure, against health-related claims |
| NSF/ANSI 401 | Emerging compounds: up to 15 claims covering prescription and over-the-counter drugs, herbicides and pesticides | The same three-part structure |
| NSF/ANSI 61 | Drinking water system components | What a component leaches into drinking water |
Three consequences for anyone planning a line
- Material safety means that your resin and carbon supply chain are included within the certification.
- Structural integrity means the cartridge has to withstand pressure which is a result of the forming process you are purchasing.
- Certifications pertain to the individual product, meaning a certified cartridge of 10 inches does not certify your 20 inch cartridge.
Certification bodies are not limited to one organization. NSF, IAPMO, WQA and UL Solutions all operate accredited programs against these standards, and the micron band you intend to sell decides which standard you end up testing to.
From Enquiry to Commissioned Line
1
Enquiry
Every enquiry is answered within 24 hours by someone who has read your specification.
2
Configuration
We provide a line configuration and a proforma along with the ancillary machines that your specification requires.
3
Order
30% T/T deposit releases the build slot.
4
Build and run-off
The line is assembled and test-run at our factory against your cartridge specification.
5
Balance and shipment
The balance is done prior to shipment, and the line is crated for ocean freight along with its documentation.
6
Commissioning
Installation assistance and startup support, with technical service reachable directly.
What a quotation for imported equipment should cover
A United States law firm that handles China equipment disputes sets out seven questions a buyer should settle before paying.[3] They make a good test of any quotation, including ours.
The danger is thinking you contracted directly with a factory and learning during a dispute that your actual counterparty is an intermediary with little control over production.
Harris Sliwoski LLP, on the first of the seven questions
The second most common mistake in this area is a structural mistake and not a legal mistake. Buying standalone machines instead of the line the plant actually needs is a recurring entry on production-line purchasing checklists. This is what The Second Machine Question tries to address. Filter cartridge making machine manufacturers publish output in pieces per day and almost never publish the cartridge weight behind this, which is the same problem one step upstream.
01
Who exactly are you buying from
02
What exactly are you buying
03
How will you know it works before it leaves China
04
How much is unpaid when you test it
05
Can you import, install and use it
06
Who will keep it running
07
What happens if it does not perform
Where our quotation answers it
The proforma invoice names Suzhou UDTECH Technology Co., Ltd. and the bank account is in that name. You are not contracting with an agent.
Where our quotation answers it
The configuration lists model, extruder and die count, bore and outer diameter, length set, micron band, and every ancillary machine as its own line.
Where our quotation answers it
The factory run-off, against your cartridge specification. Ask for the test protocol and what counts as a pass, and put it in the contract.
Where our quotation answers it
Stated plainly: the balance settles before shipment, so testing happens at our factory and not on your floor. That is why the run-off protocol belongs in the contract and why factory inspection support is quoted.
Where our quotation answers it
Supply voltage and frequency, panel approval route and floor area are quotation items. The core extrusion line alone needs a minimum of 30 square meters.
Where our quotation answers it
Spares position at order stage: die and spinneret parts on the melt blown line, cam and traverse parts on the winder, screw and barrel parts on the carbon line.
Where our quotation answers it
12-month warranty from delivery, with acceptance criteria set by the run-off protocol agreed before the build starts.
ERRORS
Where Each Line Is the Wrong Choice
Three duties that these machines should not be sold into, and one family of products that we do not manufacture at all.
Melt blown
Incorrect
This line is the wrong choice when your customer specifies an absolute rating with a defined level of efficiency at a defined particle size. Nominal rating cannot be substituted for absolute rating, and the two cannot be used interchangeably on a purchasing specification.
Where to look instead
A pleated line, which we do not manufacture.
String wound
Incorrect
This line is the wrong choice when the work is fine polishing before a membrane and the customer is sensitive to fiber shedding. With this specification, winding buys you dirt holding capacity and costs you fine polishing capability, and the single pass data above shows how much retention moves with yarn selection.
Where to look instead
Melt blown for the fine end. Wound deserves some credit on dirt-holding capacity and for use in the pre-treatment of reverse osmosis, where the spun filter manufacturing machine vocabulary is standard.
CTO carbon block
Wrong Duty
Wrong when your customers need industrial throughput. Carbon block does carry documented particulate reduction claims under NSF/ANSI 42[2], but that standard's scope is point-of-use and point-of-entry systems, and certification requires a stated filter capacity per cartridge. It does nothing for a duty measured in cubic meters per hour.
Where to look instead
Melt blown or wound for industrial pre-filtration.
Pleated cartridge production is outside our scope.
It is a different equipment family built around media and a supporting cage rather than around formed fibre: pleating, seam welding and end-cap infrared welding. If that is what you need, machines on this page are not applicable.
01 / 04
Filter Cartridge Production Evaluation Tools
01
Which cartridge line fits what you sell
Four answers, one shortlist. The model behind it is stated below the result, so you can disagree with it on the record rather than guess what it did.
02
The Changeover Tax, in hours
All three lines are described as customizable. What that word costs differs by a factor of sixteen between them, and this puts a number on it before you commit to a machine.
03
Energy per 1,000 cartridges
A running kilowatt figure means nothing until you divide it by what the line actually made that day. This does the division on one line at a time, which is the only comparison that holds.
What does a filter cartridge making machine cost?
Price follows the configuration: throughput tier, dimensional range, automation scope, electrical package and documentation. Platform listings for this class run roughly USD 20,000 to USD 50,000 per machine, and where your configuration falls within this range is decided by those five factors. If you send us the cartridge you intend to manufacture, we will give a specific figure rather than a range that fits nobody.
Which of the three machines should I buy first?
The one that makes the cartridge your customers already purchase. There isn’t just one correct first machine: melt blown covers the widest sediment market, wound handles dirt-holding and reverse osmosis pre-treatment, and carbon block takes taste and odor in point-of-use products. Send us your target cartridge specification and your target output, and we’ll inform you which line fits, including when the answer is a line that we do not make.
What is the second machine a cartridge plant usually needs?
An end-cap and adapter welding machine, more often than a second forming line. Melt blown and wound lines ship producing double open end cartridges, so every 222, 226, fin and single open end format your customers order needs a capping operation the forming line does not perform. That is The Second Machine Question, and answering it at quotation costs less than answering it after delivery.
How many cartridges per day will a line actually make?
The melt blown line is published at 3,500–4,200 pieces per 24 h on the 2E&2M and 5,000–5,800 on the 3E&3M, and the carbon block line at one 10 inch cartridge every 50–60 seconds. Piece counts on melt blown are a mass flow rate wearing a piece-count label, because cartridge weight is adjustable across 70–200 g and doubling the weight roughly halves the pieces. Ask us, and every other supplier, which cartridge weight and length the figure is calculated at.
Will these lines run on a United States power supply?
Standard supply is AC 380 V / 50 Hz or 220 V / 50 Hz and other voltages are configurable on request, but voltage is only half the question. Workplace electrical equipment in the United States must be approved under 29 CFR 1910.303(a), which 29 CFR 1910.399 resolves to acceptance by a nationally recognized testing laboratory[1], and a CE mark does not meet that requirement. Settle voltage, frequency, drive configuration and the panel approval route on the quotation rather than at commissioning.
How is the micron rating controlled on each line?
Everything that varies for melt blown involves die-to-collector distance, temperature and pressure of the hot air, mandrel rotation and push-forward speed, held by the control system. For wound, variation is dependent on the choice of yarn, winding tension, and the number of layers and the number of traverses. A published paper demonstrated a fifteen-fold difference in retention with the same winding parameters due to the choice of yarn. For carbon block, variation is dependent on the grade and particle size of the carbon and the ratio of the binder.
What certification will the cartridges need for the United States market?
That depends on the claim you intend to sell. NSF/ANSI 42 covers aesthetic effects such as chlorine, taste and odor, NSF/ANSI 53 covers health-effect claims such as lead and cysts, and NSF/ANSI 61 covers what a component leaches into drinking water. All three attach to the finished cartridge and the system, and all three test material safety, structural integrity and the specific reduction claim, none of which a machine can hold on the cartridge's behalf.
Which industries buy the cartridges these lines make?
The treatment of pure water for production, circulating cooling water, drinking water, lab water, boiler water and oilfield injection water, chemical water, pharmaceutical, electroplating, printing, paint, fuel oil and the beer and beverage industries. The main application for carbon block filter cartridges is drinking water filter products for both point-of-use and point-of-entry. The great range of applications is attributed to polypropylene itself, whose chemical flexibility covers acid, alkali and neutral duties rather than a narrow band of chemicals.
Can I change cartridge diameter after the line is installed?
Yes, and the cost differs sharply by line, which is what The Changeover Tax measures. Melt blown takes a matched mandrel shaft anywhere in 10–150 mm, and wound takes a core change plus a traverse adjustment. Carbon block needs screw and barrel parts replaced, because one extruder makes one bore and outer diameter combination, so two diameters in production usually means two extruders.
Equipment from China has a reputation for breaking down. What is different here?
Nothing about the country of origin answers that, and buyers who say it on manufacturing forums are usually describing breakdowns, software problems and slow support rather than a bad first week. The answers that do carry weight are the ones you can hold us to: the line is assembled and test-run at our factory against your cartridge specification before it ships, the run-off protocol and its pass criteria go in the contract, the spares position is set at order stage, and there is a 12-month warranty from delivery. Ask any supplier for those four in writing and compare the answers rather than the reputations.
Is there enough margin in producing cartridges rather than buying them?
That is probably the most common question for these lines, and we should really put numbers behind that question instead of just estimates. Industrial filtration people say publicly that plants pay more than one hundred dollars per big cartridge. That’s why private-label production is attractive to many people. But let’s substitute numbers here. Raw materials are the biggest part of a cartridge plant’s cost, utilities are single digits, and the machine is a single investment against margin per cartridge, so your resin and carbon sourcing matters more than the machine price does.
What is the lead time and how does payment work?
The string wound winder is scheduled at 30 working days, while melt blown and carbon block lines are quoted against your specification because output tier and tooling change the build. Payment is a 30% T/T deposit to release the build slot with the balance settled before shipment, and letters of credit are accepted. Minimum order is 1 set, with a 12-month warranty from delivery.
Do you supply the machines that make the cores and finish the cartridges?
Yes, the UDF tube making machine extrudes PP cores at 20 kW per set with a 1.5 m by 13.5 m footprint, the full-automatic gluing and capping machine welds end caps at AC 220 V / 50 Hz and 2000 W under PLC and HMI control, and a wrapping machine applies the non-woven outer layer on carbon cartridges. Together with the three forming lines that covers stages one to four of The Chain Before the Cartridge.