Get in touch with Suzhou UDTECH Technology Co., Ltd. Company

Filter Cartridge Production Lines for PP, CTO and Wire-Wound Cartridges
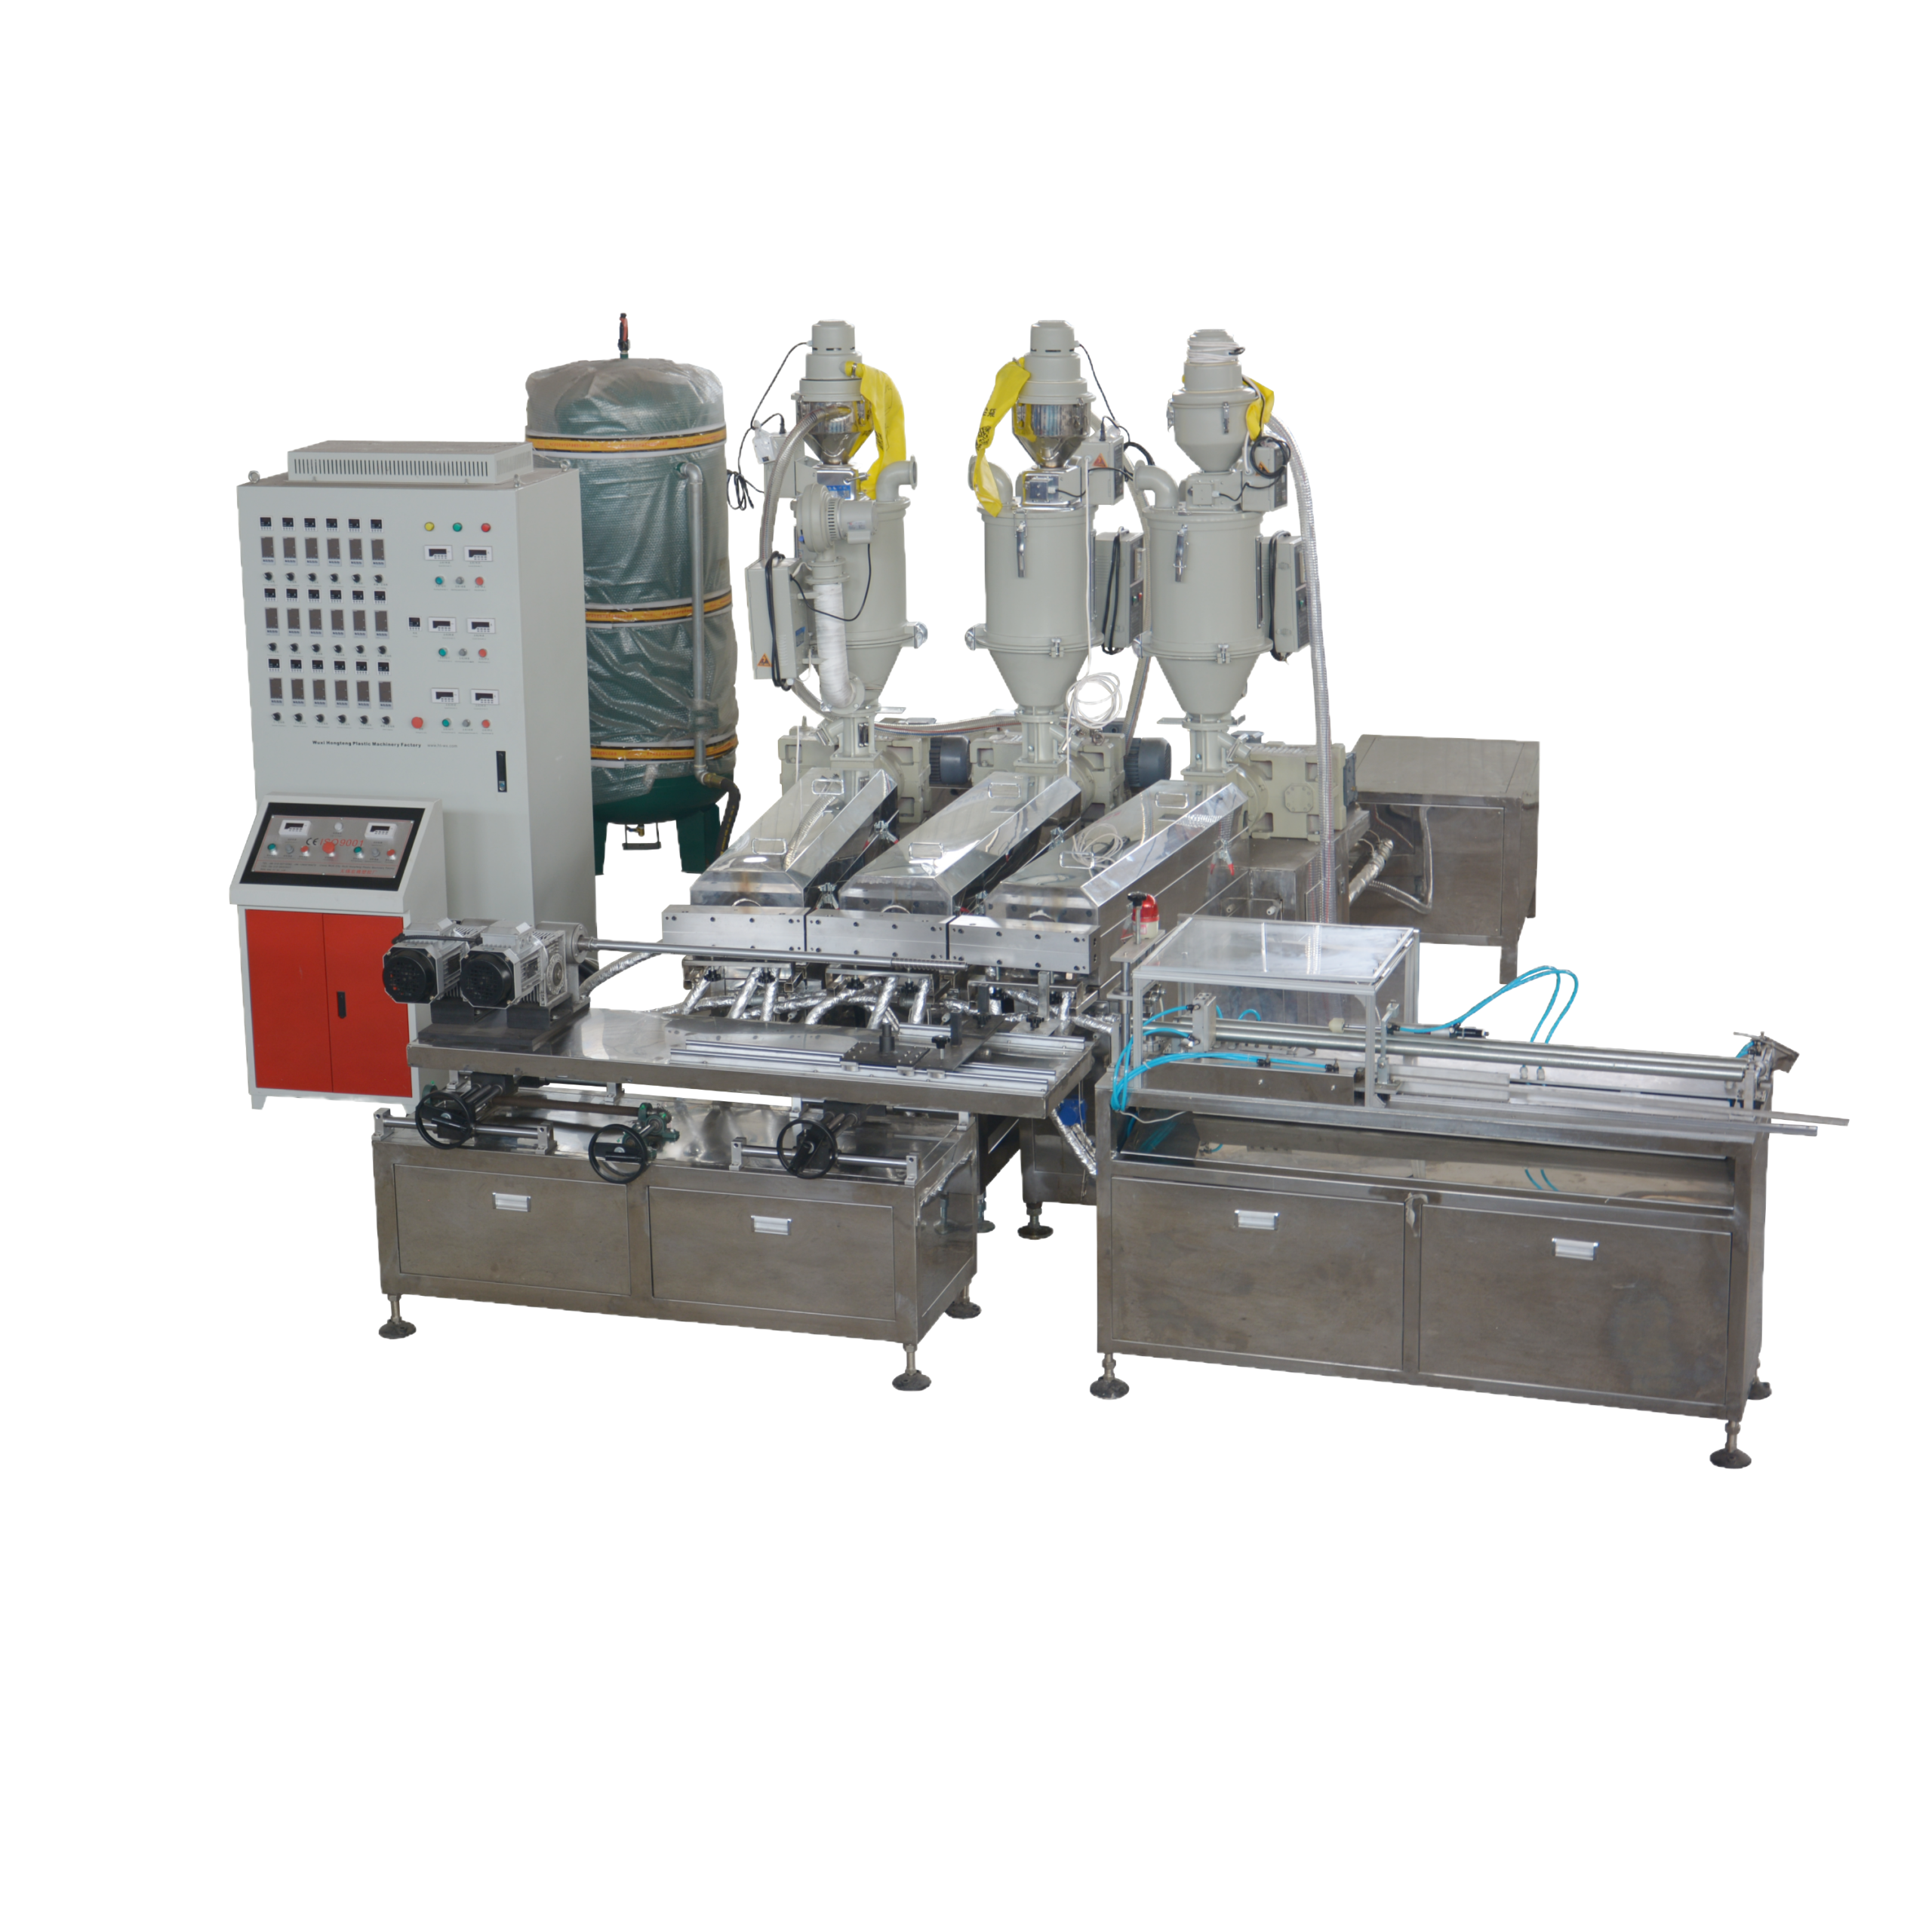
A filter cartridge production line should start with the cartridge you need to sell, not a machine label. UDTECH manufactures PP melt-blown filter production lines, CTO activated-carbon filter production lines and wire-wound filter machines, then configures the line around the finished-product brief, plant conditions and agreed supply boundary.
Application-and-Route Screening Matrix
The first decision is not “automatic or manual.” A buyer can choose the wrong route by starting with a broad machine label instead of the cartridge construction, duty and intended performance claim.
PP melt-blown route
Screen when the product brief calls for a depth cartridge formed from polypropylene fibres.
CTO carbon-block route
Screen when adsorption media, binder, block formation and powder handling define the product.
Wire-wound route
Screen when yarn, core material, winding pattern and finished diameter define the cartridge.
Potential fit
The construction and available raw materials align; product and site details still need review.
Validate first
The cartridge uses mixed media, an unusual core, a special claim or a wide changeover range.
Not enough information
The inquiry names only water treatment, micron or output without a finished-cartridge specification.
-
End use: drinking-water treatment, process liquid, reverse-osmosis pretreatment, chemical duty or another defined application.
-
Contaminant or duty: sediment loading, taste and odour objective, process protection or another stated removal task.
-
Performance objective: the finished-cartridge claim the buyer plans to validate and publish.
-
Applicable basis: customer specification, test method, certification program or destination-market requirement.1
-
Hydraulic basis: target flow rates, allowable pressure drop, housing interface and service conditions.
-
Factory basis: utilities, material storage, ventilation, operator flow, downstream operations and available floor layout.
| Application signal | What it tells the engineering review | What remains open |
|---|---|---|
| Sediment and particle removal in water filtration | A depth-filter route can enter the shortlist when PP melt-blown construction is approved. | Particle distribution, dirt load, flow rates, pressure drop, housing and micron ratings still need a test basis. |
| Taste, odour or purification objective | An activated carbon filter cartridge can enter the shortlist when adsorption media and block construction are approved. | Carbon source, binder, geometry, contact conditions and the finished-product claim remain product decisions. |
| Process-liquid protection with a string wound filter | A wound route can enter the shortlist when yarn and core construction match the duty. | Chemical compatibility, core materials, yarn, winding pattern, pressure drop and service conditions remain open. |
Configuration release rule: The screening matrix narrows the process family, but it is not a substitute for engineering review of the actual cartridge drawing or sample, raw materials, target output basis and acceptance needs.
UDTECH project review workflowThree Line Families, Three Control Problems
Our filter equipment range covers three distinct cartridge-manufacturing routes. We keep the parent-page comparison at system level so that process-specific parameters, tooling and operating detail can be confirmed for the selected child configuration.
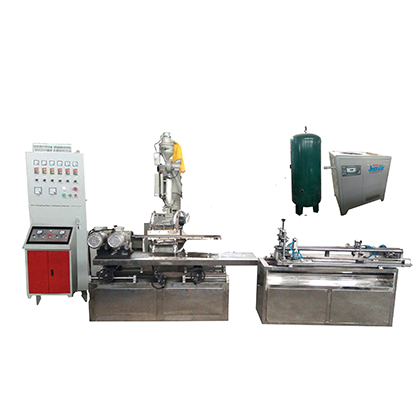
This route converts polypropylene feedstock into a formed depth-filter cartridge through material feeding, melting or extrusion, air-assisted fibre formation, receiving or winding, and cutting. The filter machine configuration follows the cartridge length, inner and outer diameter, target weight, density profile, micron objective, material grade and required automation by operation.
- Confirm polypropylene grade and any approved additive.
- Define cartridge element geometry and coreless or supported structure.
- State target mass, density profile and cut-length method.
- Identify utilities, polymer-heating controls and downstream handling.
Potential fit
Choose this route when melt-blown PP is already the approved finished-product construction.
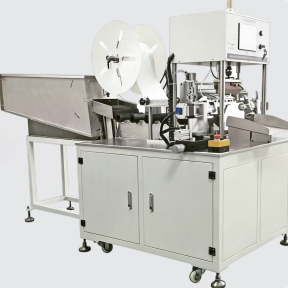
This route handles activated carbon, binder and the chosen forming method to create a carbon-block filter cartridge. The carbon filter cartridge machine must be configured around media recipe ownership, particle behaviour, block geometry, curing or cooling needs, dust control, cutting and any wrapping or end treatment.
- Confirm carbon source, particle specification and binder system.
- Define CTO carbon block geometry, mass and structural target.
- Identify recipe control, feeding, mixing and material-containment needs; keep combustible-dust review site-specific.3
- Separate forming, cutting, wrapping, inspection and packaging scope.
Validate first
A claimed chlorine, odour or organic-compound result belongs to the finished-cartridge validation plan, not the machine name.
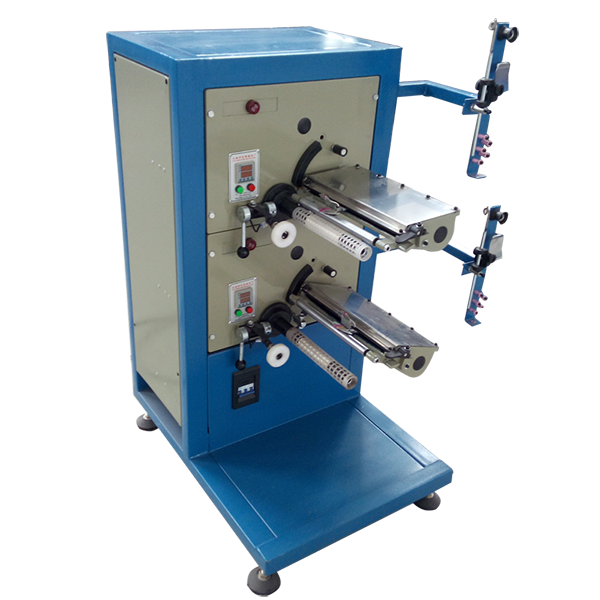
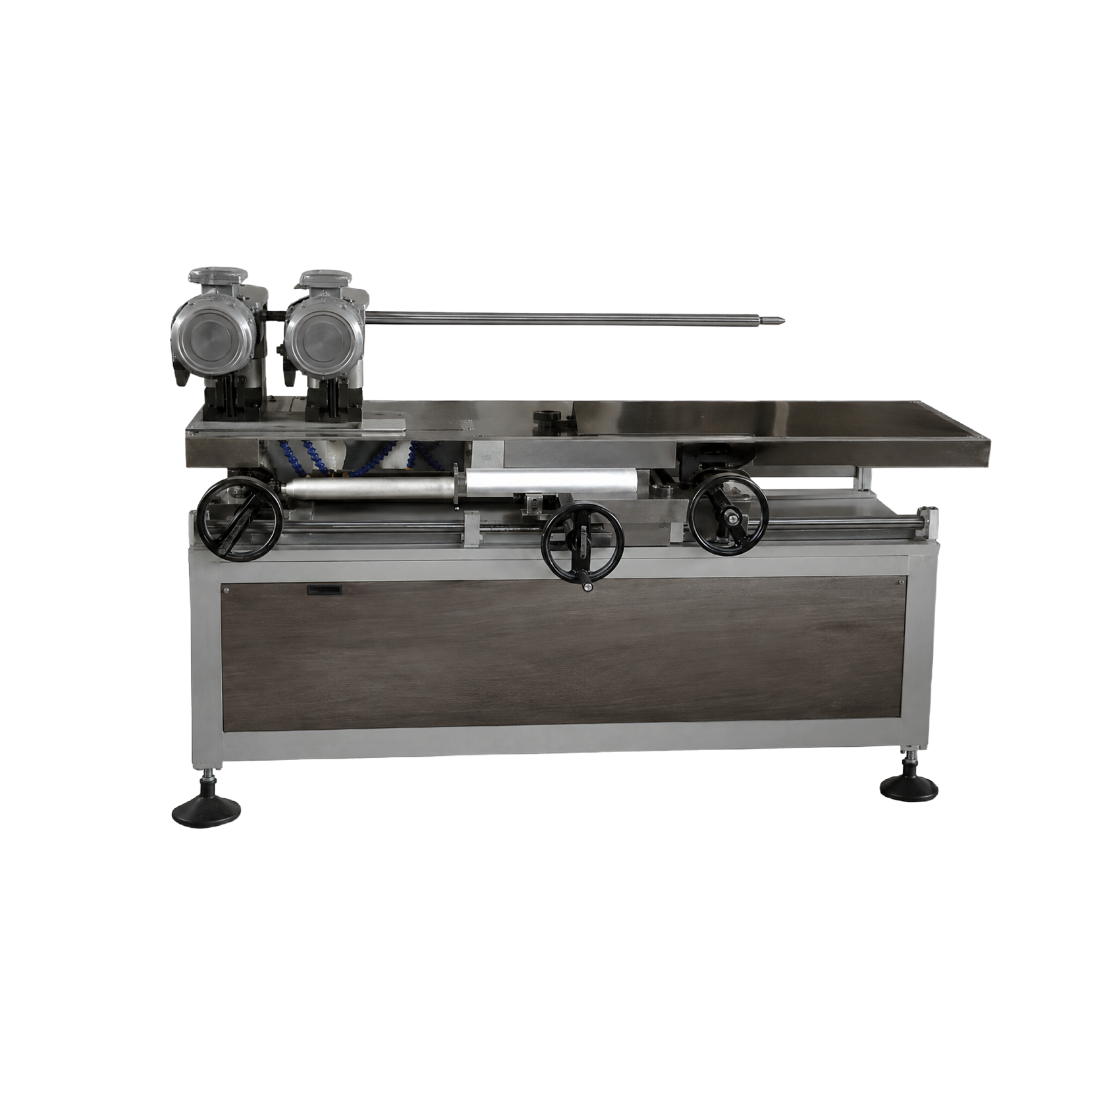
This route winds filtration yarn around an approved inner core to create the required pattern, diameter and length. The winding machine configuration follows the yarn type, core materials, tension strategy, traverse or pattern, cut-off method, operator loading and the desired level of automatic handling.
- Confirm PP yarn or other approved yarn and its supply format.
- Define core material, diameter, length and end condition.
- State winding pattern, multi-layer requirement and finished diameter.
- Identify loading, unloading, cutting, inspection and packing touchpoints.
Potential fit
Choose this route when wound construction is fixed and the cartridge specification can control yarn, core and pattern.
Parent-page capability boundary
| This page covers | A configured proposal covers | A future process page covers |
|---|---|---|
| Route selection, shared inquiry fields and supply-boundary logic | Named equipment, modules, controls, utilities, tooling and responsibilities | Process-specific operation, options and technical detail |
| Comparison method for realized output and acceptance | Project-specific target basis and test conditions | Family-specific product range after verification |
| Common project stages and site questions | Installation, commissioning, training and documentation scope | Operating sequence and maintenance detail |
Operational distinctions inside the three routes
PP fibre consistency
A melt-blown filter cartridge machine coordinates polymer feeding, thermal conditions, air, fibre formation, receiving motion and cutting. The product brief must connect those controls to cartridge mass, density profile and the filtration objective instead of relying on a “high precision” label.
Carbon recipe handling
A carbon block filter cartridge machine handles active carbon, binder and the approved forming route. Recipe ownership, dust control, material containment, block integrity and post-forming operations matter more than a generic full-automatic claim.
Winding geometry
A string wound filter cartridge machine coordinates yarn presentation, tension, traverse, core rotation, pattern build and cut-off. A filter winder that suits one core and product length is not automatically the right winding machine for a multi-layer range.
Commercial Terms: Modules and Boundary of Supply
A production line is more than its forming machine, but the common assumption that “line” means every upstream and downstream operation is not necessarily correct. We map each module as core, optional, buyer-supplied or proposal-confirmed so competing quotations can be read on the same basis.
A modular scope can be the right call when the cartridge is stable but a downstream interface still needs validation. The proposal must still identify every handoff and responsible party.
| Line stage | Buyer input | Configuration question | Proposal status |
|---|---|---|---|
| Raw-material storage and feeding | Material grade, form, packaging and handling limits | Which transfer, drying, dosing, mixing or containment steps are required? | Confirm equipment and responsibility |
| Primary forming | Approved cartridge construction and dimensional brief | Which forming process, number of positions, tooling and controls match the product? | Confirm core machine |
| Cutting and end preparation | Length, end geometry and tolerance | Is cutting inline, separate or handled after conditioning? | Confirm module and interface |
| Joining or wrapping | End-cap, adapter, wrap and sealing requirement | Does the product need hot melt, ultrasonic weld, thermal joining or another approved method? | Confirm after sample review |
| Inspection and sampling | Drawing, test basis, sampling plan and records | Which checks belong in the line and which belong in the buyer’s laboratory? | Confirm acceptance boundary |
| Transfer and packaging | Pack format, hygiene need and downstream destination | Is operator transfer acceptable, or is an automated interface required? | Confirm downstream scope |
Process Interfaces and Downstream Operations
The finished cartridge can require more than forming. Cutting, end treatment, adapter or end-cap joining, outer wrap, marking, inspection and packaging must be connected to the primary process without assuming that every operation belongs in one machine frame. For CTO powder handling, dust collection remains a site-specific process interface rather than an assumed part of the core machine.3
State the approved cartridge length, end condition, cut quality and any allowance for later joining. The proposal then identifies whether cut-off is inline, indexed or handled as a separate production process.
End cap, adapter, outer cage, housing interface and seal geometries are determined by the completed filter element. The ultrasonic, thermal, infrared, adhesive or hot-melt processes are considered only if the joint design is compatible with approved materials.
Dimensional checks, mass checks, visual inspection, sampling, traceability, lab testing and final packaging are separate decisions. We define the required records and operator touchpoints before they are priced as line scope.
Automation by operation
The trade-off is that extra automation can reduce a defined operator task while adding interfaces, changeover work and acceptance points. “Automatic” is not always a reliable full-line description unless each operation and remaining touchpoint are named.
| Operation | Automation question | Human decision that remains |
|---|---|---|
| Material loading | Manual charge, assisted transfer or controlled feeding | Material verification, lot release and replenishment |
| Forming and control system | Recipe, PLC sequence, speed coordination and alarm handling | Start-up approval, process response and deviation review |
| Transfer | Operator move, gravity path, conveyor or robotic handling | Quality hold, jam response and changeover release |
| Inspection | Inline sensor, gauge station or laboratory sampling | Acceptance decision and disposition of nonconforming product |
From machine output to a saleable cartridge
Cartridge manufacturing output becomes useful only after the required cut, joint, inspection and packing handoff is complete. For industrial liquid filtration, the assembly line should also keep material identity, accepted-product status and rejected-product handling visible from the core forming step to the agreed release point.
Line Configuration Input Checklist
Configuration starts when a broad inquiry becomes a controlled product brief. We use the checklist below to connect the cartridge, raw material, output target, factory conditions and acceptance method without filling missing fields with assumptions.
Specification group
What to send
-
Finished-cartridge structure
PP melt-blown, CTO carbon block or wire-wound; include a drawing, sample or controlled product specification.
-
Application and filtration objective
End use, process liquid, contaminant or duty, target micron language, flow basis and allowable pressure drop.
-
Cartridge dimensions
Length, inner diameter, outer diameter, core, end geometry, adapter, seal and housing interface.
-
Material system
Polymer grade, activated-carbon and binder specification, yarn, core material, wrap, cap and approved substitutions.
-
Output basis
Product format, target weight, shift hours, changeover mix, planned stops, scrap basis and included downstream work.
-
Quality and acceptance
Applicable test, customer standard, sample plan, records, trial material, acceptance duration and sign-off responsibility.
-
Utilities and site
Voltage and frequency, power availability, compressed air, water, extraction, ventilation, layout and environmental limits.
-
Project handover
Installation boundary, commissioning, operator training, language, documentation, spares and support expectations.
Two output figures are not comparable when the suppliers use different cartridges, operating calendars or handoff points. NIST's manufacturing KPI framework is a general indicator taxonomy, not a filter-line performance standard; its throughput, availability, productivity, quality and maintenance measures are not interchangeable, and the project-specific comparison basis comes from the buyer's own conditions.
| Comparison field | Hold constant | Reason |
|---|---|---|
| Finished product | Length, diameters, weight, construction and micron objective | A lighter or shorter cartridge is not the same production task. |
| Operating calendar | Shift hours, start-up, planned stops and unplanned downtime | Nameplate speed does not include lost production time. |
| Product mix | Changeover frequency, range and cleaning or purge sequence | Frequent changes reduce available running time. |
| Quality yield | Scrap definition, rework and accepted-product count | Total pieces and accepted pieces are different outputs. |
| Test window | Warm-up, trial duration, material lot and acceptance rules | A short demonstration can hide stability or changeover losses. |
| Scope boundary | Forming only versus cutting, joining, inspection and packaging | Output at different handoff points is not directly comparable. |
Commercial Terms and Scope Confirmed in the Written Proposal
Price follows the process family, product range, forming positions, tooling, automation, controls, auxiliaries, downstream modules, acceptance scope, service boundary, destination and documentation. There is no useful fixed price for a line until those fields describe the same project.
Quotation drivers
| Driver | Why it changes the quotation | Input that removes uncertainty |
|---|---|---|
| Cartridge range | More lengths, diameters, materials or structures can change tooling and changeover design. | List current products and planned extensions separately. |
| Automation scope | Automatic feeding, transfer, cutting, joining, inspection and packing are different work packages. | Mark each operation as manual, assisted or automatic. |
| Line boundary | Utilities, dust control, cooling, conveying and packaging can sit outside the core machine. | Use an included, optional and buyer-supplied responsibility table. |
| Acceptance basis | Trial material, run duration, product mix, records and sign-off effort affect the project plan. | Attach the acceptance objective and responsible approvers. |
| Site and destination | Electrical conditions, layout, language, documentation and travel scope affect delivery preparation. | Provide the destination and site-input sheet with the RFQ. |
Fields confirmed before order release
- Configured equipment and module list, tooling, controls and stated exclusions.
- Buyer-supplied materials, utilities, civil work, unloading and interface responsibilities.
- Price, minimum order basis, payment terms, trade terms, delivery basis and quotation validity.
- Inspection, factory trial, acceptance, documentation, installation, commissioning and training scope.
- Warranty, recommended spares, travel, remote support and other after-sales terms.
Commercial comparison sequence
- Standardize product scope - Include identical cartridge structures, dimensions, materials and product mix in every inquiry.
- Standardize machine scope - Examine core forming, auxiliaries, cutting, joining, inspection, transfer and packaging line by line.
- Standardize operating basis - Use a consistent shift calendar, changeover, maintenance, scrap and accepted-output definition.
- Standardize project obligations - Compare documentation, trial, installation, commissioning, training, spares, warranty and support as specified items.
Quality Control and Acceptance Planning
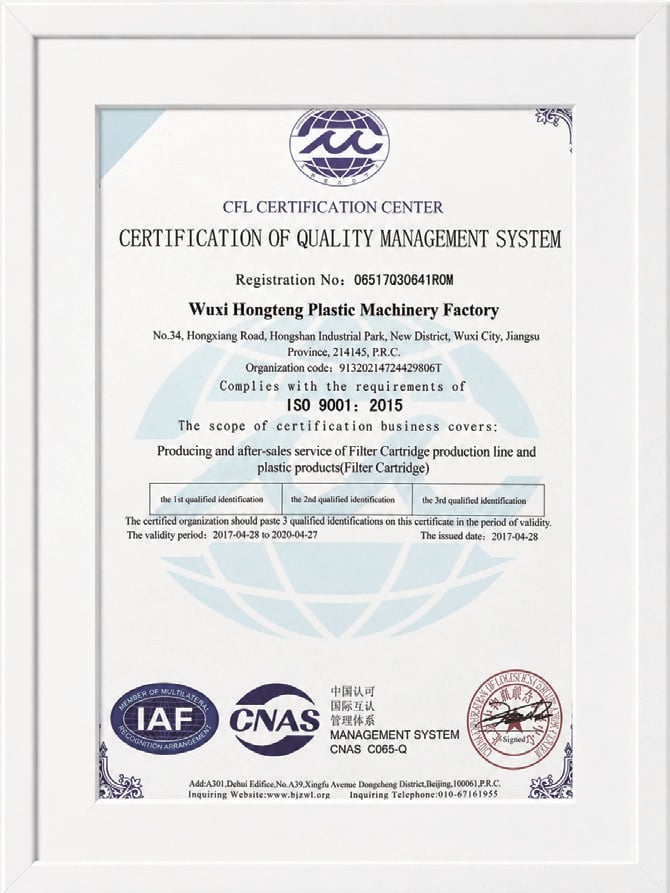
We connect machine configuration to a finished-cartridge acceptance plan before the build scope is fixed because an unclear test boundary creates acceptance risk. UDTECH's ISO 9001:2015 quality-management system applies to the company system; it is not a substitute for machine-specific acceptance or finished-product validation.
| Evidence object | Purpose | Responsibility to confirm |
|---|---|---|
| Approved drawing or sample | Controls geometry, interfaces and visible product requirements | Buyer approval and revision status |
| Raw-material specification | Controls polymer, carbon, binder, yarn, core and approved substitutions | Buyer requirement and supplier traceability scope |
| Process and control review | Connects setpoints, recipes, alarms and operator actions to the configured route | UDTECH configuration and buyer operating input |
| Factory trial plan | Defines material lot, product format, test window, changeover and output basis | Jointly agreed plan and sign-off roles |
| Inspection record | Captures agreed dimensional, mass, visual or process checks | Record format, sampling and acceptance limits |
| Open-items register | Separates completed tests from site-dependent or buyer-dependent items | Owner, due point and closure evidence |
UDTECH Manufacturing and Support Basis
Suzhou UDTECH Technology Co., Ltd. develops and produces filter equipment, including PP melt-blown filter production lines, CTO activated-carbon filter production lines and wire-wound filter machines. Our operations integrate research and development, production, domestic sales, global export and technical after-sales services.
6,000-square-meter workshop
Standardized production space with manufacturing, laboratory and testing equipment.
ISO 9001:2015
Quality management system certification; this scope does not by itself approve a machine or cartridge.
More than 55 countries
UDTECH equipment has been supplied across established export markets.
Independent development
Our research and development work is connected to equipment production and application review.
Full-process quality control
Project documents, production checks and agreed acceptance records remain connected.
Technical after-sales service
Support scope is matched to the configured project and confirmed in the proposal.
Research and development centers
Equipment development is connected to product-route and application review.
Skilled professional teams
Engineering, production, quality and service roles support the equipment project.
Manufacturing, laboratory and testing equipment
Facility resources support equipment production and agreed verification work.
Proof matched to the decision
- Use the quality-system certificate to evaluate management-system scope.
- Use the configured proposal and equipment records to verify the scope of supply.
- Use the acceptance and factory trial records to verify the agreed-upon scope of the machine.
- Use the relevant product test or certification route to verify completed-cartridge claims.
SYSTEM TOOLS
Engineering Evaluation Tools
FAQ: Filter Cartridge Production Line Questions
Which line is used for PP melt-blown, CTO carbon block and wire-wound cartridges?
PP melt-blown cartridges use a fibre-forming route based on polypropylene; CTO carbon blocks use carbon, binder and a block-forming route; wire-wound cartridges use yarn wound around a core. Start with the approved finished-cartridge construction, then validate its material, dimensions, duty and site conditions.
What information is needed to configure a filter cartridge making machine?
Identify the water filter or process application, cartridge construction, dimensions, materials, micron or performance goal, pressure drop basis, target weight, product mix, output basis, utilities, downstream scope, and acceptance procedure. A drawing, sample, and controlled material specification eliminate assumptions.
How should production capacity be compared between suppliers?
Hold the cartridge length, diameters, weight, structure, accepted-product definition, shift hours, downtime, changeover, maintenance, scrap, test duration and downstream handoff point constant. Compare realized accepted output on that shared basis, not the highest isolated speed figure.
Can one line make multiple cartridge lengths, diameters or micron grades?
The answer depends on the selected route, tooling, receiving or winding system, cut-off method, controls and approved product range. List each required format and annual mix so change parts, recipe control and changeover work can be evaluated in the proposal.
Which utilities and factory-space inputs are needed before quotation?
Provide voltage, frequency, available power, compressed air, water, extraction, ventilation, ambient limits, floor layout, access and connection points. CTO powder handling also needs a site-specific combustible-dust and housekeeping review; PP and winding routes need their own heat, air, guarding and material-flow checks.
What does automatic include on a production line?
Specify automation separately for feeding, forming, transferring, cutting, joining, inspecting, and packing. Detail operator interactions including loading, replenishment, sampling, changeover, responding to alarms, quality release, and handling nonconforming product.
Which downstream modules may be separate from the core machine?
Cutting, trimming, end-cap or adapter joining, wrapping, outer-cage assembly, marking, inspection, conveying and packaging can be separate modules. Their inclusion depends on the cartridge design, material compatibility, target handoff point and required operator flow.
What should installation, commissioning and operator training include?
Confirm layout and foundation inputs, utility connection, unloading, positioning, approved trial material, commissioning sequence, operator roles, language, documents, spares and sign-off stages. The written proposal assigns each task and separates factory-complete checks from site-dependent work.
How should acceptance be defined for a configured line?
Use the approved cartridge specification, raw material, trial format, operating window, changeover condition, inspection record, accepted-output basis, open-items register and named approvers. Finished-cartridge performance, filtration efficiency or water purification certification remains a separate validation task unless its test is explicitly included.
What does the written proposal confirm about price and delivery?
It identifies the equipment and module list, tooling, controls, exclusions, buyer-supplied items, price, payment terms, trade terms, delivery basis, acceptance scope, installation, commissioning, training, warranty, support and validity. Only the configured proposal sets UDTECH's project-specific values and obligations.
Is an active carbon cartridge line the same as a CTO line?
Active carbon is often used as broad shorthand, while CTO usually points to a carbon-block cartridge intended for chlorine, taste and odour applications. The approved carbon, binder, geometry, forming route and performance claim decide whether the requested equipment is the same production task.
Can the same machinery cover every industrial filter cartridge?
No. This parent page covers PP melt-blown, CTO carbon-block and wire-wound routes; pleated membrane, high-flow pleated, air-filter and other cartridge constructions can require different filter media, pleating, welding, outer cage, sealing and manufacturing equipment.