Get in touch with Suzhou UDTECH Technology Co., Ltd. Company

A gradient density melt blown filter cartridge is a depth-filter element that uses a deliberately changing fibre and void structure through its wall, usually with a more open upstream zone and a tighter downstream zone. That design has the potential to improve the loading of particles through the media. However, simply having this design doesn’t prove micron efficiency, pressure drop, or dirt-holding capacity.
From the perspective of a production-line buyer, the significant question is whether the supplier can link polymer, line settings, a finished-cartridge structure, and application-specific tests. This guide provides a means to specify the profile and accept the result. Updated September 2026.
Direct answer
A gradient density melt blown filter cartridge should be specified by profile direction, rating basis, challenge test, fluid condition, geometry, and lot-acceptance method. Compare results only when flow, viscosity, housing, contaminant distribution, and terminal pressure conditions match.
Quick specification card
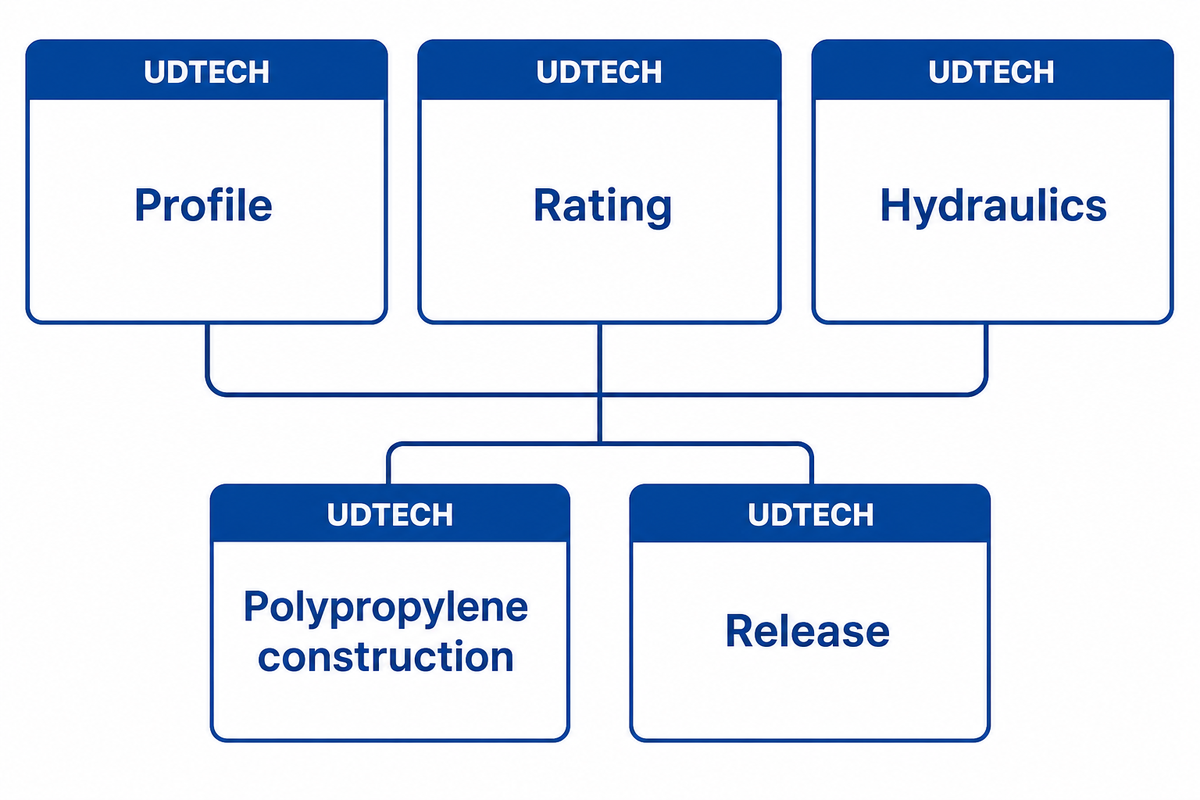
- Profile: coarse-to-fine direction and how it’s measured across the wall.
- Rating: nominal or absolute wording, target efficiency, particle challenge, and test method.
- Hydraulics: clean and loaded differential pressure at stated flow, fluid, temperature, and housing.
- Polypropylene construction: polymer grade, dimensions, mass, core or coreless form, end condition, surface finish, and groove pattern when specified.
- Release: sampling plan, traceability, nonconformance route, and change-control record.
Key points for buyers
- A smaller micron number can raise clean pressure drop or shorten usable loading headroom.
- A visible density gradient is structural evidence, not a filtration-efficiency result; the layered-nonwoven comparison is used only as a structure example.
- Steady-flow data can’t automatically predict cyclic-flow retention.
- Food-contact material status doesn’t certify a finished cartridge or its contaminant claims.
What “gradient density” means inside a melt-blown filter cartridge
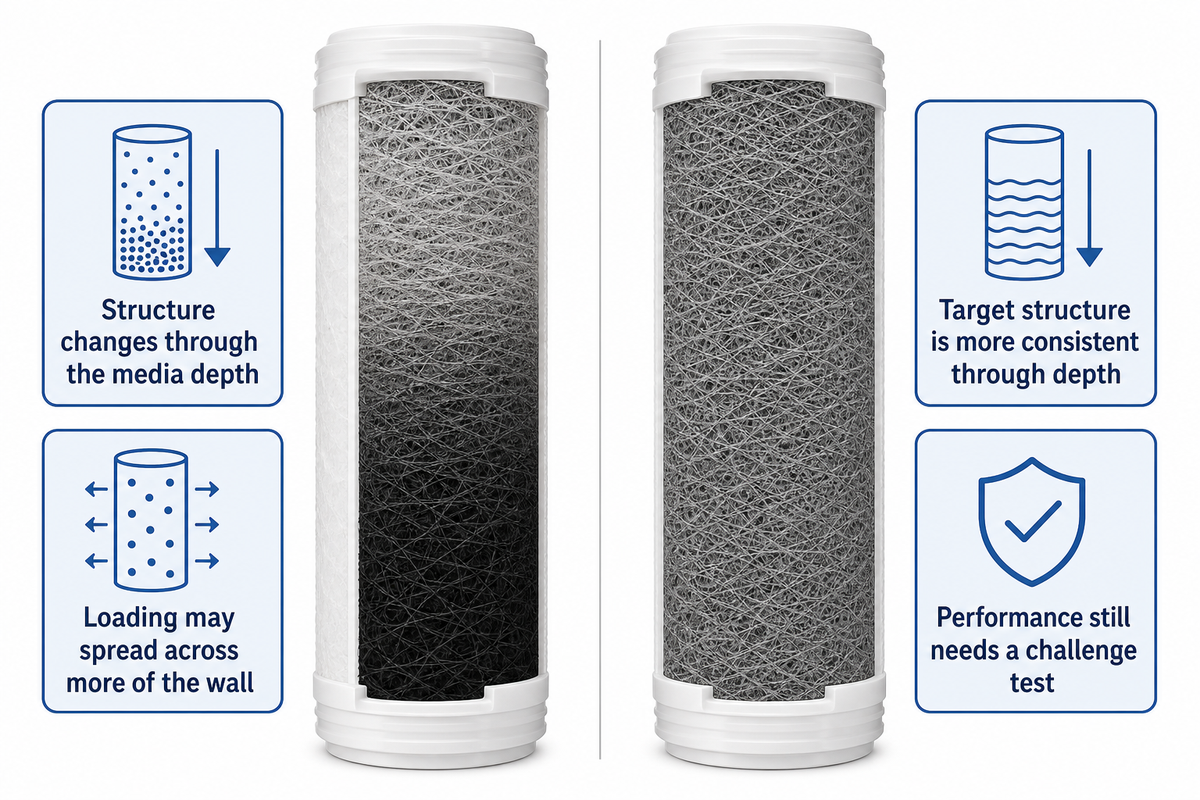
Gradient density describes a through-wall change in fibre packing and pore structure. In the common coarse-to-fine arrangement, the upstream region admits larger particles while the tighter downstream layers provide the final retention stage, but that structure alone is not a standalone efficiency rating; the layered-nonwoven comparison is used here only as structural evidence.
Gradient-density wall
- Structure changes through the media depth
- Loading may spread across more of the wall
- Profile direction must be identified
- Performance still needs a challenge test
Uniform-density wall
- Target structure is more consistent through depth
- Loading may concentrate nearer one region
- Rating basis still needs definition
- Performance uses the same evidence discipline
The term “gradient density” doesn’t define the steepness of the gradient, whether it’s radial or layered, or how consistently it’s produced. Therefore, the measurement path, range of sample variability, and definition of an acceptable profile should be clearly defined by the buyer.
Buyer objection: “The sample looks graded.” Appearance can support a process review, but a cross-section, mass profile, or another declared structural method is needed before the term becomes an acceptance condition.
How fibre diameter, polymer flow and line settings create the profile
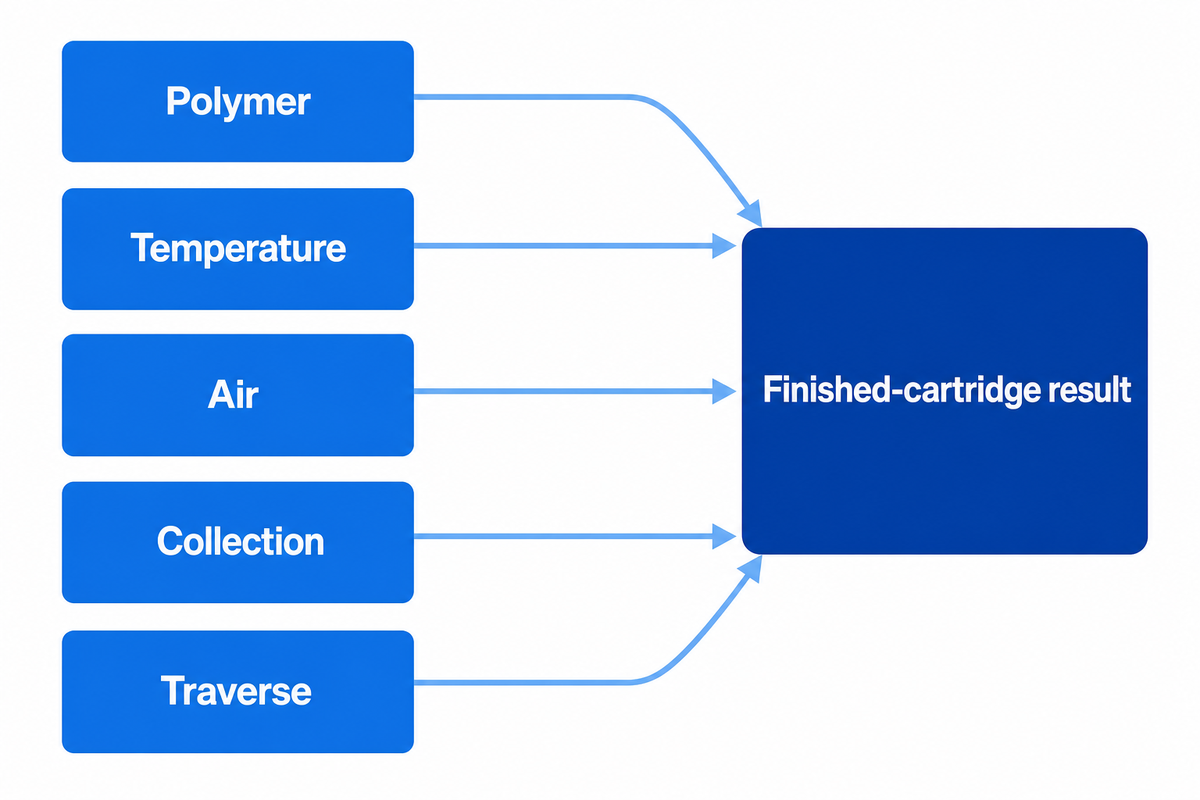
The profile is the outcome of the material, thermal, air, extrusion, collection, and traverse settings. For each approved cartridge specification, a stable recipe therefore requires linked setpoints, measured actual values, and a finished-cartridge result rather than one “best” machine setting.
0.175 g/cm³PBT calendared sample
0.088 g/cm³PP non-calendared sample
2 samplesillustration, not a line recipe
A peer-reviewed layered-nonwoven study reported calculated bulk densities of 0.175 g/cm³ for a calendared PBT melt-blown sample and 0.088 g/cm³ for a non-calendared PP melt-blown sample. Because both polymer and processing differed, the comparison only illustrates structure sensitivity; it is not a UDTECH setpoint or a prediction of liquid-cartridge life.
| Control family | Record on the line | Check on the cartridge |
|---|---|---|
| Polymer | Grade, lot, melt-flow basis | Mass and profile consistency |
| Temperature | Zone setpoint and measured value | Fibre formation and defects |
| Air | Pressure, temperature, stability | Fibre and surface consistency |
| Extrusion | Throughput and pressure trend | Mass per unit length |
| Collection | Mandrel speed | Wall build and density path |
| Traverse | Push-forward speed | Axial uniformity |
| Distance | Die-to-collector position | Bonding and surface condition |
| Cooling | Air or water condition | Dimensions after stabilization |
| Cutting | Length command and tool state | Length and end quality |
Why a coarse-to-fine path changes pressure drop and dirt holding
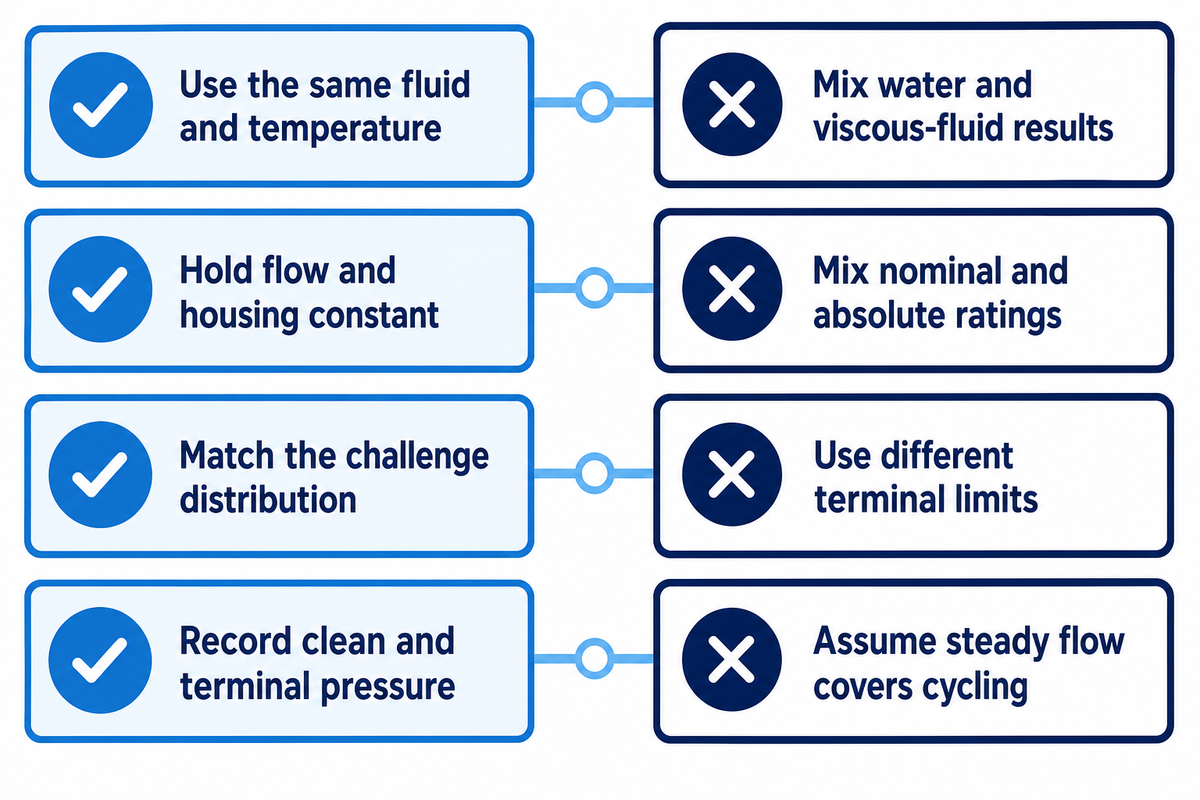
A coarse upstream zone may intercept larger particles before a fine downstream zone completes the task. Whether that arrangement lowers the rate of pressure rise or extends service life depends on the fluid, particle distribution, flow regime, housing, and stopping rule used in the test; confirm the applicable scope and edition against the official ISO 23369:2021 public record.
Compare
- Use the same fluid and temperature
- Hold flow and housing constant
- Match the challenge distribution
- Record clean and terminal pressure
Do not compare
- Mix water and viscous-fluid results
- Mix nominal and absolute ratings
- Use different terminal limits
- Assume steady flow covers cycling
Differential pressure should be plotted against the time or challenge mass that has been delivered, not reported as a single number. Retention should be evaluated within the scope of the operating pattern that matters, as cyclic flow can dislodge previously captured material.
When gradient helps and when it fails: A graded wall can distribute loading when the upstream layer remains open enough to admit part of the challenge. It can still plug early when the particle distribution, surface finish, or flow condition concentrates loading at one interface.
How to choose micron rating, nominal vs absolute, and end-use boundary
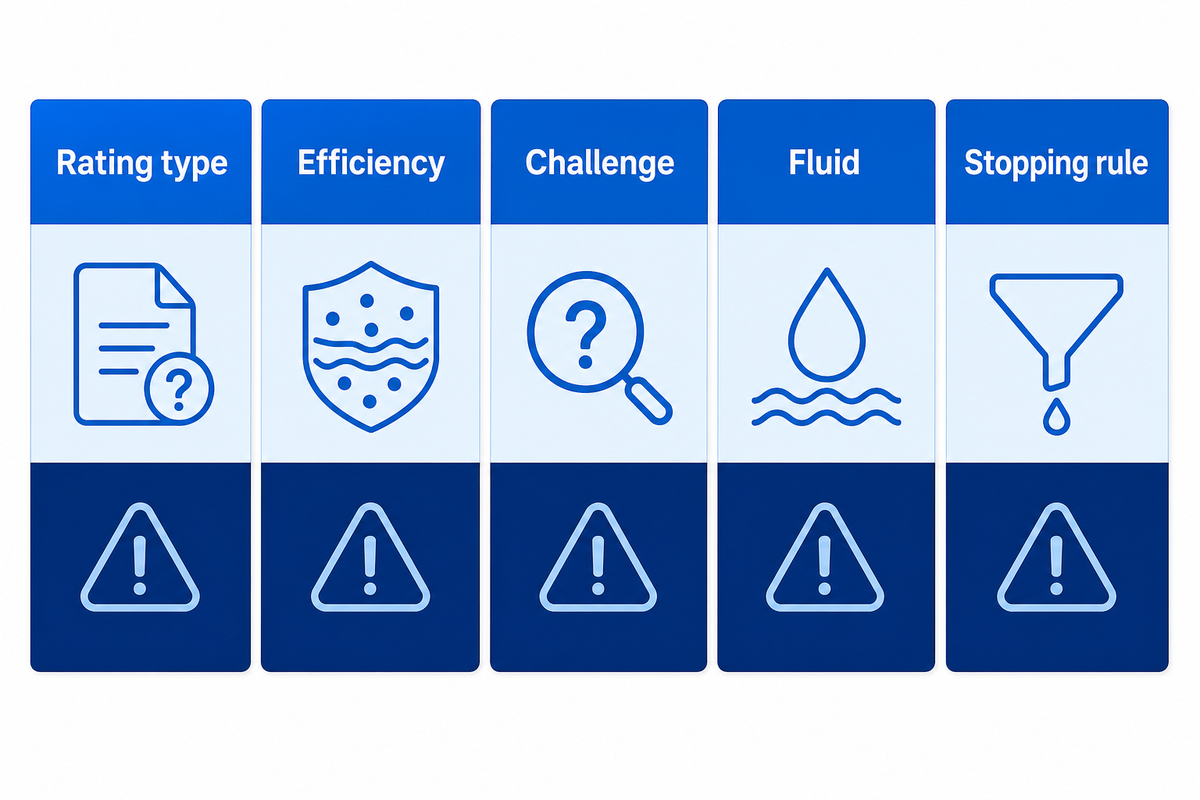
To select a micron rating, pair the pore or particle size with the stated value of efficiency and challenge material, test method, fluid, flow and cartridge geometry. “Nominal” and “absolute” are incomplete when the supplier doesn’t state the efficiency basis behind the label; verify the applicable method and edition through an official source such as the ISO 23369:2021 public record.
What micron rating should a melt-blown cartridge use?
The rating should safeguard the downstream process without imposing excessive pressure loss or frequency of replacements. This should begin with the largest particle to be restrained, the permissible downstream concentration, the process flow, and the highest differential pressure that’s acceptable; then ask for a test basis that correlates to these conditions.
Catalog vocabulary boundary: Labels such as 1 micron, 5 micron, 10 micron, 20 micron, dual gradient, sediment cartridge, sediment filter cartridge, melt blown sediment, micron sediment, nominal micron, full flow, grooved polypropylene, and micron grooved describe different catalog conventions. Rating statements still need a test basis, and the word “groove” usually describes a surface form rather than filtration efficiency.
Search results for online retail can combine topics for Big Blue/BB housings as well as for Pentair, Pentek or Aqua-Pure. Big Blue and BB are housing terms, while Pentair, Pentek, and Aqua-Pure are brand names; pleat, spin, pre-filter, and depth filtration describe different construction or duty concepts. None of those elements provides a line-acceptance method on their own.
| Field | Question to ask | Weak answer |
|---|---|---|
| Rating type | Nominal, absolute, or method-specific? | “Micron rated” |
| Efficiency | At what removal percentage? | “High efficiency” |
| Challenge | Which particle and distribution? | “Standard dust” |
| Fluid | Which liquid and viscosity? | “Water-like” |
| Flow | Per cartridge or per housing? | “Normal flow” |
| Temperature | Test and service temperature? | “Ambient” |
| Geometry | Length, diameters, end form? | “Standard size” |
| Stopping rule | Which terminal pressure or time? | “Until blocked” |
| Lot release | How many samples and which failures? | “Random inspection” |
The 5-Step Gradient-to-Evidence Fit Check
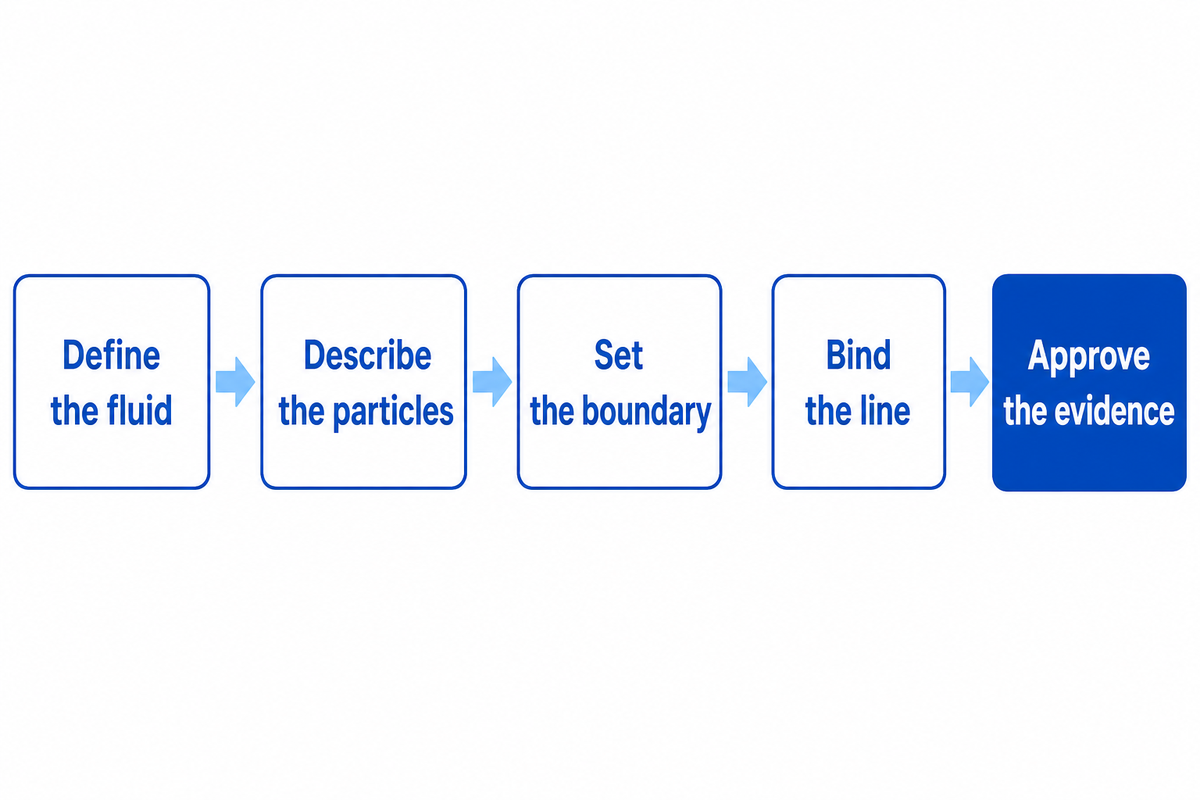
The 5-Step Gradient-to-Evidence Fit Check links the process need to a testable cartridge and line specification. It prevents a buyer from selecting equipment around one micron label while leaving fluid, geometry, utilities, and acceptance evidence undefined; this follows the measurement-first discipline reflected in NIST manufacturing guidance.
- Define the fluid: record chemistry, viscosity, temperature, cleaning, and contamination limits.
- Describe the particles: state the size distribution, shape, deformability, and loading pattern.
- Set the boundary: identify rating basis, efficiency, pressure limit, and service endpoint.
- Bind the line: connect polymer and operating records to the required cartridge geometry and profile.
- Approve the evidence: name the tests, sample plan, witnesses, records, and nonconformance route.
A gradient design is an option when the challenge presents a meaningful spread of particle sizes and the loading test yields a useful distribution through the wall. A uniform design may be preferable when the separation duty is narrow and the buyer demands an easier structural target.
The 5-Field Cartridge Acceptance Matrix: approve one row each for fluid condition, particle challenge, cartridge geometry, line recipe record, and functional test result. Capex reviewers can then compare suppliers on the same evidence instead of comparing adjectives.
Production-line controls that must be visible in a supplier discussion
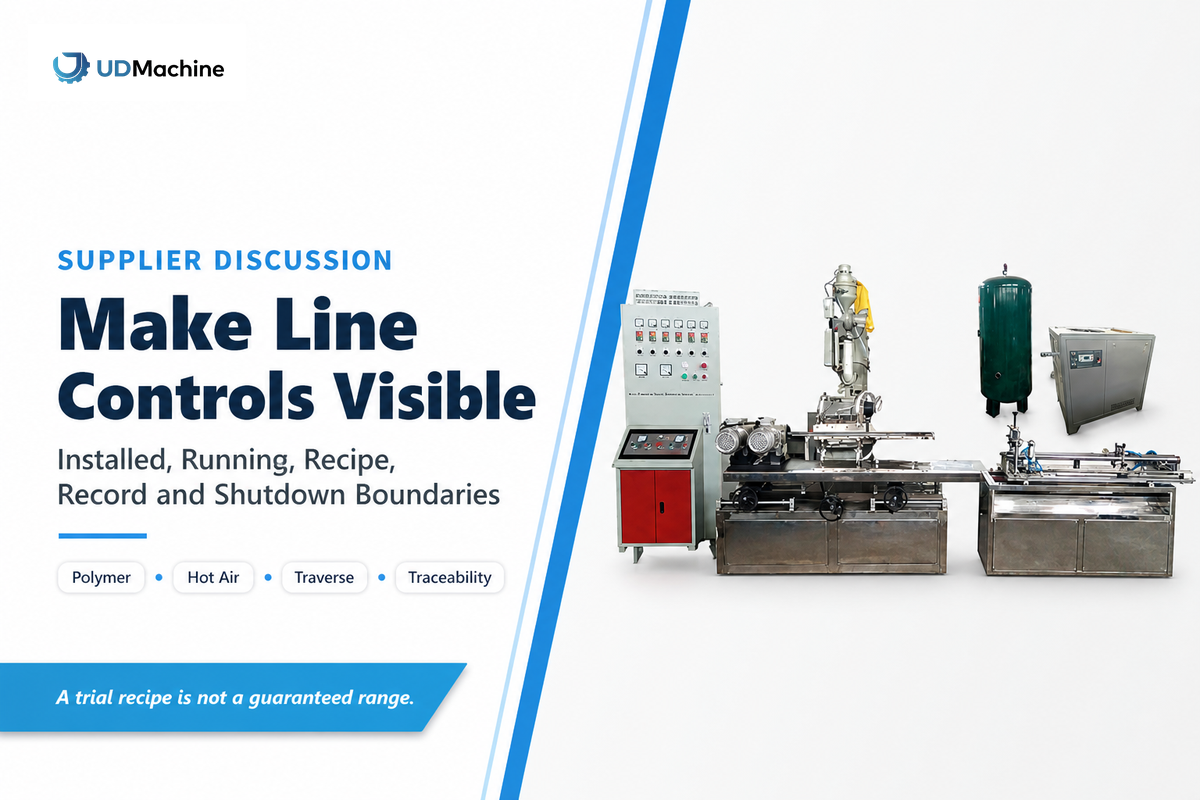
A useful supplier discussion connects target cartridge geometry and profile to polymer handling, melt delivery, hot-air control, collection speed, traverse, cooling, cutting, and traceability. The proposal should distinguish installed values, running values, and values that remain subject to the approved product recipe.
Ask the supplier to identify which controls are recipe-based, which are set manually, which are recording controls, and which controls shut down the production line. For line configuration context, review the PP melt-blown filter cartridge production line and return the RFQ with your intended cartridge and utility basis.
Supplier discussion boundary
Don’t treat connected power as normal running power, a maximum mechanical speed as saleable output, or one trial recipe as a guaranteed range. Record each value with its operating condition and acceptance owner.
The broader range of filter cartridge production line solutions allows for the separation of PP melt-blown equipment from carbon-block and wire-wound devices. Separation is justified because the evidence and process parameters can’t be substituted.
Acceptance testing: prove the profile, not just the appearance
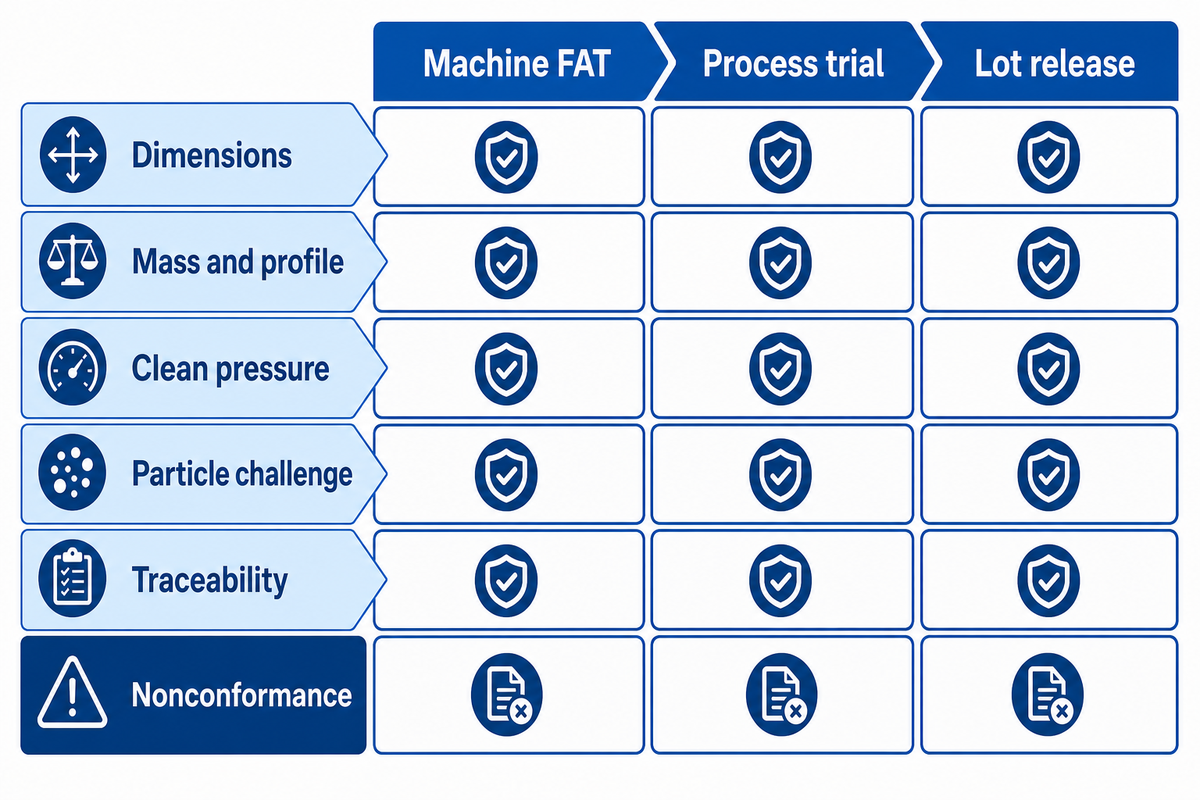
Acceptance should consist of three consecutive layers: machine factory acceptance, witnessed process trial, and finished-cartridge lot release. Structural measurements will ascertain whether the intended cartridge was manufactured; functional tests will determine whether that cartridge fulfills the declared filtration specification, while the official ISO 2942:2018 scope page defines the separate fabrication-integrity and first-bubble-point boundary.
| Evidence item | Machine FAT | Process trial | Lot release |
|---|---|---|---|
| Safety and interlocks | Witness functions | Confirm recipe access | Review alarm records |
| Utilities | Record supply basis | Record running values | Check drift records |
| Dimensions | Confirm measurement tools | Measure trial pieces | Apply sampling plan |
| Mass and profile | Agree method | Map cross-section | Trend by lot |
| Clean pressure | Confirm test rig boundary | Test stated fluid and flow | Check release sample |
| Particle challenge | Agree protocol | Run functional test | Use approved method |
| Cyclic condition | Define when applicable | Observe retention | Retain exception record |
| Traceability | Review data fields | Bind sample to recipe | Bind result to lot |
| Nonconformance | Agree decision owner | Classify trial failure | Hold, rework, or reject |
While a bubble-point or profile test can indicate a structural concern, it does not evaluate filtration effectiveness or contaminant capacity. Keep the structural result adjacent to, rather than in place of, the functional challenge record.
Assignment rule: Every failed result needs a named owner and evidence path. Without that rule, a line supplier, polymer supplier, test laboratory, and cartridge producer can each apply a different explanation to the same failed run.
Applications, chemical boundaries and when another media wins
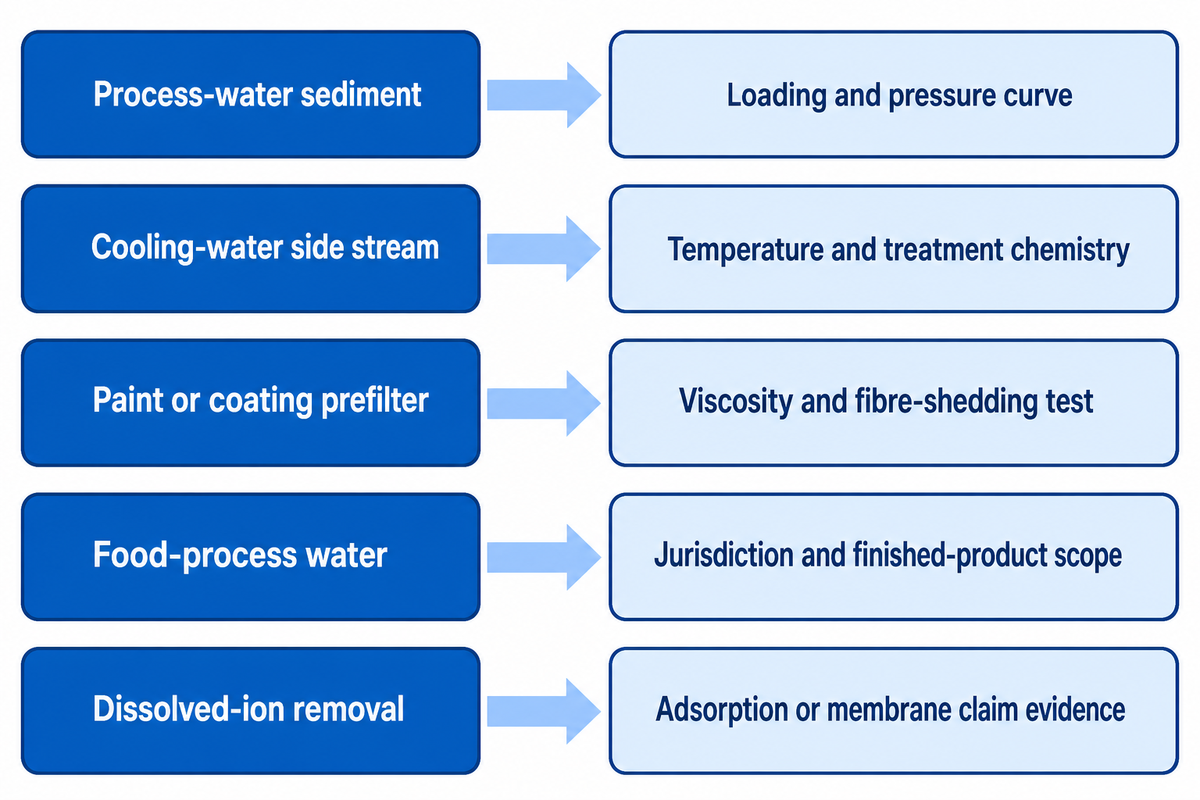
Polypropylene melt-blown media commonly serves suspended-particle removal, but chemical resistance and application fit depend on chemistry, concentration, temperature, contact time, cleaning, and required purity. A high level of purity also requires evidence of extractables, leachables, rinse-up, and variation of lots.
Compatibility evidence boundary: One pipe-grade polypropylene study used 5 mg/L free chlorine at 60 °C for up to 2,000 hours and reported about 30% longer time to embrittlement for one grade. The result shows why grade and exposure matter, but it cannot predict melt-blown cartridge service life.
| Application type | Possible role | Evidence needed |
|---|---|---|
| Process-water sediment | Depth prefiltration | Loading and pressure curve |
| Well-water sediment | Variable-particle prefilter | Seasonal challenge sample |
| Cooling-water side stream | Particulate control | Temperature and treatment chemistry |
| Paint or coating prefilter | Agglomerate removal | Viscosity and fibre-shedding test |
| Electroplating bath | Suspended-solid control | Chemical compatibility by condition |
| Food-process water | Claim-specific prefiltration | Jurisdiction and finished-product scope |
| Pharmaceutical utility | Conditional prefilter | Extractables, rinse-up, bioburden plan |
| Analytical sample preparation | Only after contamination review | Blank, leachables, lot variation |
| Dissolved-ion removal | Usually another medium | Adsorption or membrane claim evidence |
“May be safely used as articles or components of articles intended for use in contact with food, subject to the provisions of this section.”
This definition applies to qualifying olefin polymers in the context of the conditions stated herein. It does not verify a completed cartridge, a production line, or a claim for contaminant reduction.
Reject vague comparison language: “Superior chemical resistance” and “economical replacement” are incomplete without the chemical, exposure, test method, service endpoint, and ownership cost boundary. Taste, odor, and rust claims also need the applicable finished-product test rather than a resin or machine statement.
RFQ checklist: the fields that prevent an expensive re-run
A useful response to an RFQ outlines the cartridge, the criteria for evaluating the line, and the evidence required to satisfy the order. It distinguishes settled requirements from requirements that still need to be assessed, either through a trial or engineering evaluation.
RFQ checklist: copy these fields into your quote request.
| Parameter | Requested basis | Why it matters | How to verify |
|---|---|---|---|
| Cartridge geometry | Length, OD, ID, end form | Defines tooling and handling | Drawing and measured samples |
| Rating basis | Efficiency, challenge, method | Prevents micron ambiguity | Approved test protocol |
| Profile target | Direction and measurement path | Defines “gradient” | Cross-section or agreed method |
| Output basis | Saleable cartridge definition | Avoids speed-only claims | Witnessed timed trial |
| Utilities | Voltage, air, cooling, exhaust | Protects site integration | Utility schedule and running log |
| Controls | Recipe, alarm, access, export | Supports repeatability | PLC demonstration and record |
| Acceptance | FAT, trial, lot-release split | Assigns evidence ownership | Signed acceptance matrix |
| Support | Training, spares, response route | Defines post-handover scope | Named deliverables and contacts |
Suzhou UDTECH Technology Co., Ltd. reports a 6,000 m² standardized workshop and exports to more than 55 countries. Those company facts can support due-diligence questions about manufacturing and service reach, but they do not replace a project-specific FAT, cartridge test, or support agreement.
Buyers can review UDTECH’s wider filter cartridge making machines context, then use the exact PP line configuration resource for the commercial discussion.
Evidence and regulatory scope buyers should track in 2026
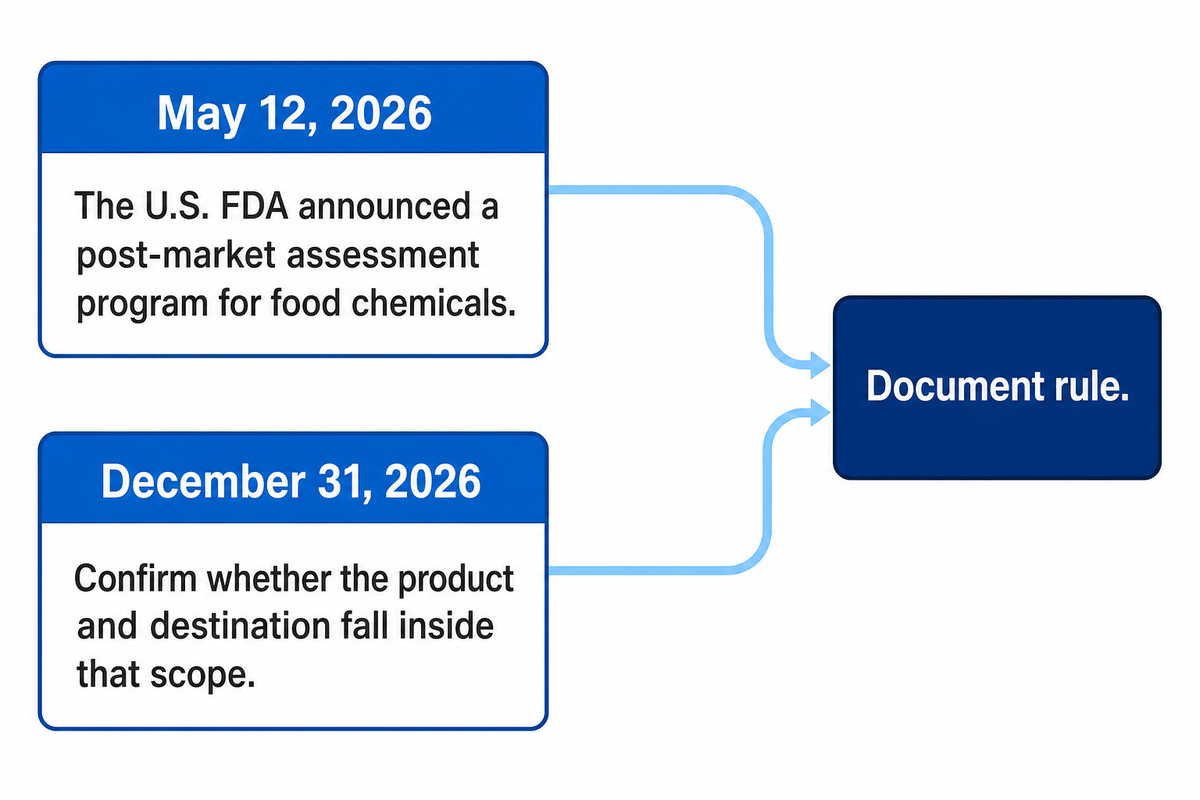
The relevant 2026 change isn’t a proven market trend for this exact cartridge term. Buyers should track dated regulatory processes, jurisdiction, applicable material or product scope, conditions of use, and document revisions.
May 12, 2026
The U.S. FDA announced a post-market assessment program for food chemicals. Treat it as a dated evidence-process development, not a generic approval for polypropylene cartridges.
December 31, 2026
EU Regulation 2024/371 applies its marking specifications to in-scope products that contact water intended for human consumption. Confirm whether the product and destination fall inside that scope.
The procurement file should capture the version or revision of each requirement and who made the determination on its applicability. When the destination or the intended use differs, reopen the review of the scope rather than upholding an old approval.
| Recorded value | Source context | Allowed use in this guide |
|---|---|---|
| 0.175 g/cm³ | PBT calendared sample | Illustrates structure sensitivity |
| 0.088 g/cm³ | PP non-calendared sample | Not a cartridge target |
| 35–1,200 g/10 min | Published process-property range | Literature context, not a line limit |
| 2–18 Pa·s | Published viscosity context | Literature context only |
| 5 mg/L | Pipe-grade chlorinated-water study | Shows exposure specificity |
| 60 °C | Same degradation study | No cartridge-life transfer |
| 2,000 hours | Same degradation study | Study duration only |
| 30% | Reported grade difference | Directional, not predictive |
| 0.880–0.913 g/cm³ | 21 CFR 177.1520 material criterion | Resin scope only |
| 160–180 °C | 21 CFR 177.1520 material criterion | Not a process recipe |
| 6.4% and 9.8% | Listed extractable-fraction limits | No finished-product certification inference |
| 6,000 m² | User-supplied UDTECH workshop fact | Company context only |
Document rule: record the jurisdiction, substance or product, manufacturer, intended use, test conditions, revision date, and responsible reviewer. A logo or certificate title without that context is not enough for technical acceptance.
Frequently asked questions
How does a gradient density melt blown filter cartridge differ from a uniform-density cartridge?
Answer
A gradient cartridge changes fibre packing or pore structure through the wall, while a uniform-density cartridge targets a more consistent structure. The gradient may distribute a broad particle challenge through more media depth, but the claimed advantage must be checked at the same flow, fluid, housing, challenge, and terminal pressure.
Is a smaller micron rating always better for a PP melt-blown cartridge?
Answer
No. A tighter rating can increase clean differential pressure, concentrate loading, or shorten service time when it’s finer than the process requires. Select the rating from the downstream protection target and verify its efficiency basis under the intended fluid and flow conditions. Compare the tighter option against the current cartridge using the same challenge and stopping rule.
What information should a supplier provide before I buy a production line?
Answer
Request the target cartridge definition, supported polymer and recipe boundary, utility schedule, control and traceability fields, saleable-output basis, factory acceptance procedure, process-trial plan, training, spares, and support route. Mark every unconfirmed item as subject to engineering review or a witnessed trial. Ask who owns each test record, how a failed acceptance point will be closed, which documents are included at handover, how recipe access is controlled, and which operating values the line records automatically.
Can PP melt-blown cartridges be used with chemicals?
Answer
Compatibility depends on the chemical, concentration, temperature, exposure time, stress, cleaning, and the exact polypropylene grade. For high-purity use, also assess extractables, leachables, rinse-up behaviour, and lot variation under the actual service conditions. A 5 mg/L, 60 °C, 2,000-hour pipe-grade study with a 30% difference can’t be treated as a cartridge service rating.
How should FAT results be connected to finished-cartridge quality?
Answer
Bind each FAT sample to its polymer lot, recipe, measured operating values, dimensions, mass or profile result, and functional challenge result. The signed record should also state which criteria belong to machine function, which belong to process capability, and which belong to finished-lot release. Keep the sample identification with the test report.
Turn the profile into an acceptance plan
Send your cartridge drawing, fluid and particle description, rating basis, required output basis, utilities, and test plan to UDTECH. The technical team can review the production-line boundary before a recipe or performance commitment is discussed.
Evidence note
This guide separates published research, regulatory scope, first-party company information, and project-specific acceptance evidence. Illustrative study values aren’t UDTECH specifications, and no application should be approved without checking the actual fluid, operating conditions, cartridge construction, and applicable requirements.
References & Sources
- 21 CFR 177.1520, Olefin polymers U.S. Electronic Code of Federal Regulations
- Standards for Water Treatment Systems NSF
- Layered nonwoven composite structure research PubMed Central
- Polypropylene degradation under chlorinated-water exposure PubMed
- ISO 2942:2018 scope page International Organization for Standardization
- ISO 23369:2021 public record International Organization for Standardization
- ASTM D543-21 scope page ASTM International
- FDA food chemical post-market assessment program U.S. Food and Drug Administration
- Commission Delegated Regulation (EU) 2024/371 EUR-Lex